Golf ball manufacturing process time depends more on the production route than on layer count or machine speed. At Golfara, many standard production runs move through roughly 13–16 days of active manufacturing stages from core molding through final QC, while customer-facing planning windows are wider.
A fast molding or printing cycle does not mean the whole batch is finished quickly. Golf balls still move through conditioning, cover forming, surface finishing, coating, printing, inspection, and final release, with corrective work added if a quality gate fails.
Machine Cycle Time and Batch Manufacturing Time are not the same clock. For buyers, the useful number is how long the complete routed batch takes to reach final manufacturing release—not how fast one machine completes a single operation.
Manufacturing process time is also different from OEM order lead time, which can include approvals, pre-production scheduling, holidays, production-slot timing, and other order-level delays.
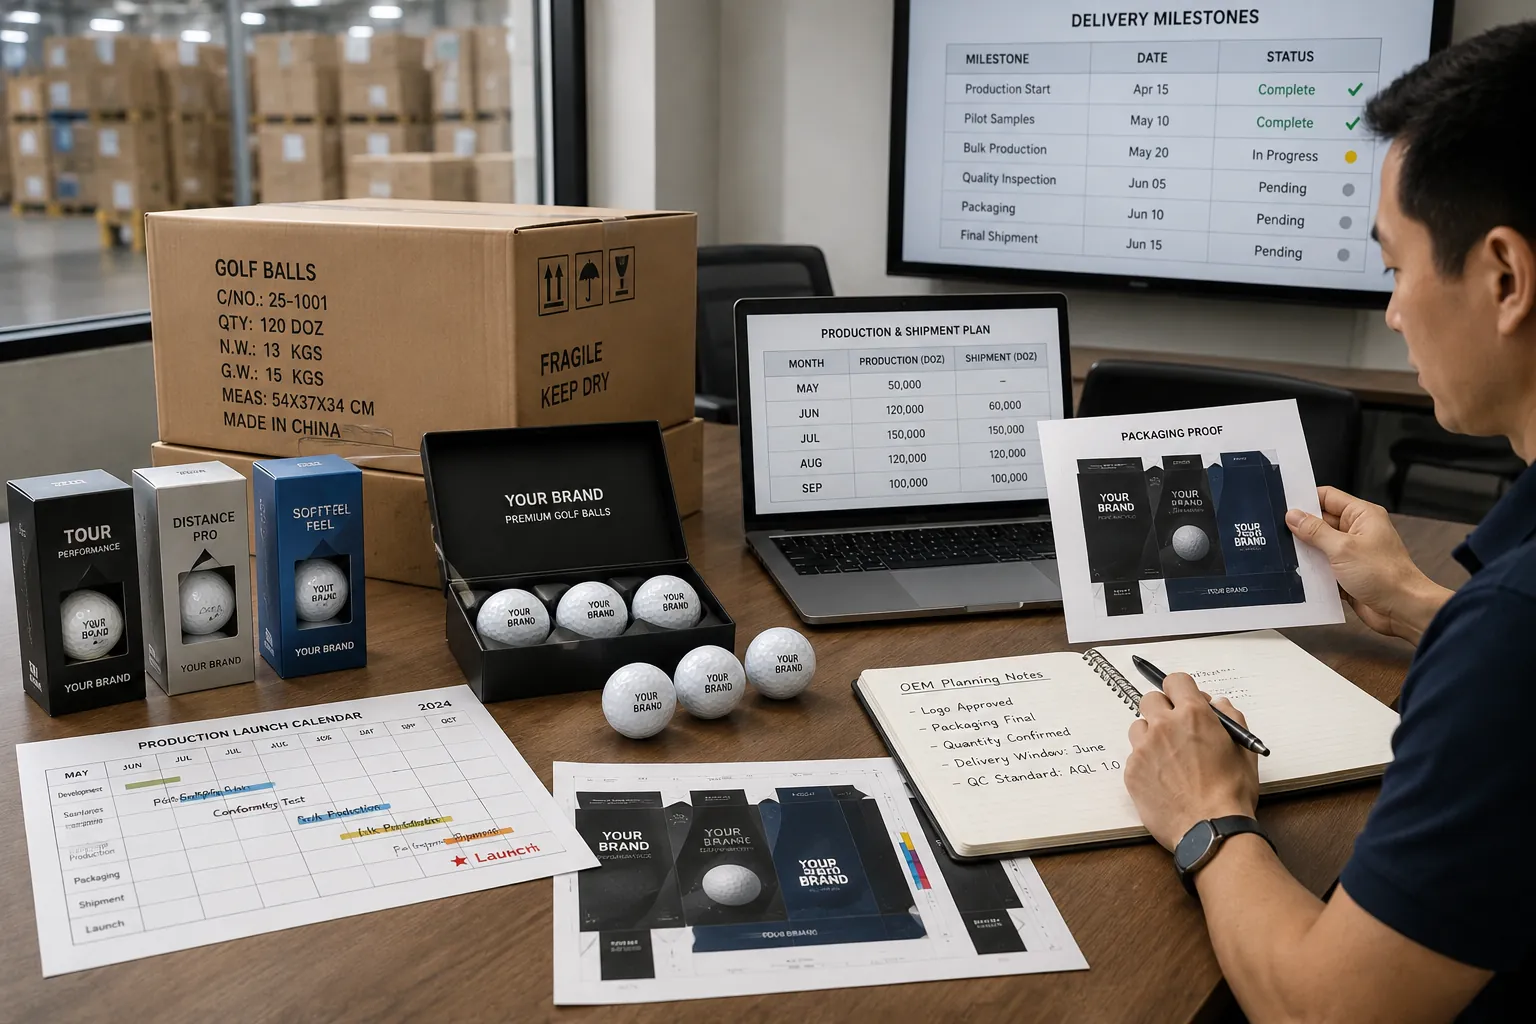
What Actually Sets Golf Ball Manufacturing Time?
You may see a fast molding cycle or a large daily-capacity number and wonder why a 10,000-ball batch is not finished almost immediately. The missing piece is routing.
A molding machine may complete one operation quickly, but your batch still has to pass through repeated production cycles and downstream stages. Machine Cycle Time multiplied by order quantity is not a reliable formula for Batch Manufacturing Time because machine speed measures one operation while batch time measures the routed process to manufacturing release.
Machine Cycle or Batch Manufacturing Time?
For procurement, it helps to separate four different clocks. The first three explain what happens inside manufacturing; the fourth belongs to the broader OEM order calendar.
| Pain / decision | Clock | What it measures | Action / evidence |
|---|---|---|---|
| “How fast is the machine?” | Machine Cycle | One defined machine operation | Ask what operation the figure describes |
| “How long is the batch actively processed?” | Active Manufacturing Time | Core through finishing and QC | Review the route-stage sequence |
| “Why is the planning window wider?” | Factory Flow / Planning Time | Routed stages, handoffs, corrective work and buffer | Compare planning band with active stages |
| “When will my PO be ready to ship?” | Buyer Order Clock | Approvals, queue, calendar and order timing | Move to the OEM lead-time plan |
The Lean Enterprise Institute’s cycle-time definitions support the same underlying manufacturing distinction. Machine cycle time describes the time a machine needs to complete its operations on one piece, while production lead time describes movement through the broader process from start to finish. Lean also distinguishes processing time from the longer elapsed production time.
For a golf ball buyer, that distinction matters because a molding-cycle figure describes only one operation. It cannot substitute for the routed batch time required to move your SKU through forming, conditioning, finishing, coating, printing, inspection, and manufacturing release.
Major-brand manufacturing provides a useful reality check. A public golf ball manufacturing process shows that production continues well beyond core molding through additional layers, cover formation, finishing, painting, inspection, and other controlled operations. The exact Golfara route differs by SKU, but the manufacturing principle is the same: the mold opening is not the end of the clock.
At Golfara, core molding is normally allocated about 2–3 days at the batch-stage level for applicable production routes. One core obviously does not sit in a mold for three days. That stage time covers repeated molding runs across the required quantity, loading and unloading, handling, intermediate checks, and release of the completed batch to the next manufacturing step.
The same distinction applies downstream. A cover-forming action, coating pass, or logo-printing action may be quick at the equipment level, yet thousands of balls still need to pass through the operation, be handled, inspected, conditioned where required, and released.
This is why nominal factory capacity and customer batch time answer different questions. A high throughput figure may describe one machine, one line, one construction, or aggregate factory output. It does not automatically tell you when your exact SKU will complete every required production stage.
Headline capacity presented as batch-release speed is a failure signal.
Before comparing suppliers, ask them to separate machine-cycle information, active manufacturing stages, and the customer-facing production-planning window. A supplier that can explain those clocks is giving you much more useful manufacturing evidence than one large balls-per-day number.
✔ True — High nominal capacity can coexist with a multi-day manufacturing route
Machine throughput describes one operation or capacity measure. Your batch still has to complete every required downstream manufacturing and release stage.
✘ False — “If the factory can make tens of thousands of balls per day, my order should be finished the same day”
Daily output does not tell you when your specific batch clears core production, cover forming, finishing, coating, printing, QC, and final manufacturing release.
Which Manufacturing Stages Consume Real Time?
A supplier can tell you “20 days production” without showing where those days go. That makes the number hard to compare, challenge, or explain internally.
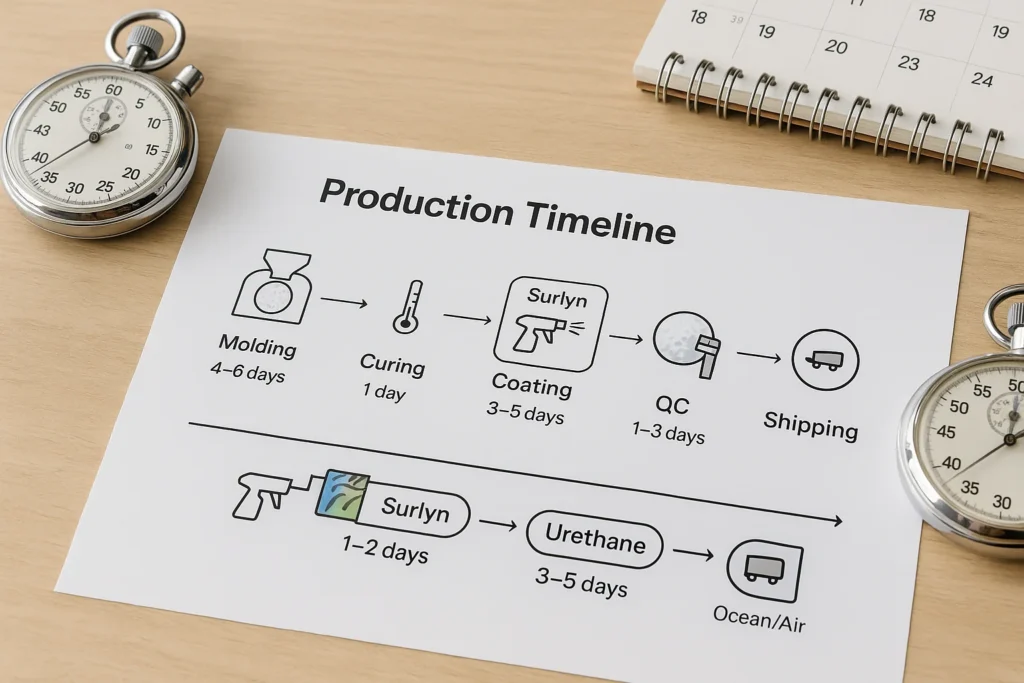
Golfara’s standard high-level route moves from core molding through conditioning, cover forming, finishing, coating, printing, and final QC. For many standard runs, those active stages add up to roughly 13–16 days, but the customer-facing planning window is wider because routed production is not one uninterrupted line reserved for a single order.
At Golfara, we separate active manufacturing-stage time from the wider planning window communicated to the customer.
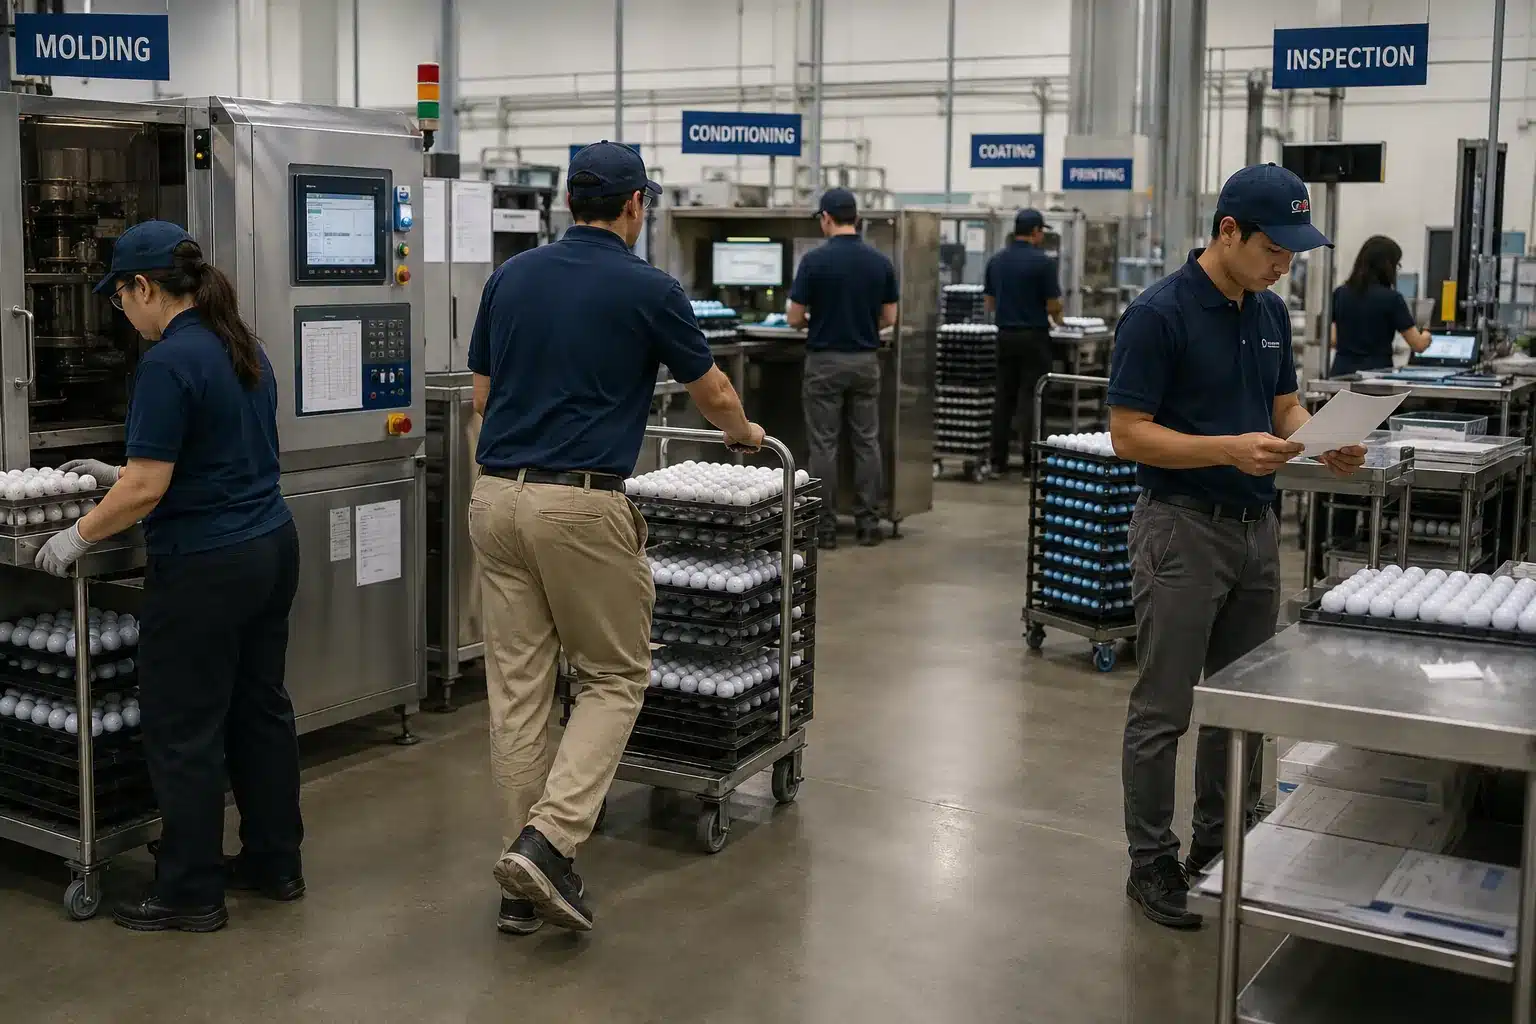
| Pain / decision | Golfara active-stage reference | What consumes the stage time | Action / evidence |
|---|---|---|---|
| Core production | 2–3 days | Repeated molding, handling, checks and release | Confirm batch-stage completion |
| Conditioning | 2–3 days | Controlled intermediate conditioning or holding | Confirm next-stage readiness |
| Cover forming | About 2 days | Approved cover-forming route | Verify actual cover process |
| Surface finishing | About 2 days | Preparation and finishing before coating | Confirm surface-stage release |
| Coating | About 2 days | Application, cure/dry, stabilization and inspection | Check coating-release status |
| Printing | About 1 day | Setup, batch printing, cure/dry and inspection | Confirm print-stage release |
| Final QC / release | 2–3 days | Inspection and release under normal conditions; holds or corrective action can extend the stage | Request final batch status |
Read sequentially, those Golfara stage references total approximately 13–16 days for many standard production runs before additional manufacturing buffer or corrective work is considered.
That is not a universal China manufacturing formula. It is a practical reference from Golfara’s own routing.
Our current customer-facing production-planning references are intentionally wider:
-
2-piece Surlyn / ionomer route: 15–25 days
-
3-piece Surlyn / ionomer route: 18–30 days
-
4-piece cast thermoset urethane route: 30–50+ days
These figures are also Golfara planning references—not an industry rule saying every 2-piece, 3-piece, or 4-piece golf ball must take the same number of days.
The difference matters.
A 15–25-day production plan does not mean golf balls spend 15–25 continuous days inside manufacturing equipment. The active stages themselves can add up to a shorter sequence, while the customer-facing planning window also allows for routed handoffs, shared production resources, route-specific processing, finishing, QC, reasonable manufacturing buffer, and corrective work where required.
A detailed Ball Plant manufacturing tour illustrates why this distinction exists. Its public process moves through conditioning, molding, intermediate layers, cover formation, buffing, surface preparation, painting, drying, printing, and inspection rather than treating molding as the entire manufacturing process.
For your sourcing team, the evidence action is simple: ask for a route-stage schedule or production traveler showing the major manufacturing steps required by your exact SKU and the release status of each stage.
Active Manufacturing Time and Customer Production Planning Time are related, but they are not the same clock.
That distinction also makes supplier comparisons fairer. One factory may give you a theoretical machine-speed figure. Another may give you a conservative batch-release window. Until both numbers describe the same clock, comparing them tells you almost nothing about which supplier actually manufactures faster.
Why Do Ionomer, TPU, and Cast Routes Differ?
Two suppliers can quote a 3-piece urethane golf ball and still be describing very different manufacturing clocks. The word urethane alone does not tell you which process is running.
A 3-piece or urethane label does not tell you the manufacturing clock by itself. Ionomer and TPU can use thermoplastic molding routes, while cast thermoset urethane relies on reactive casting and curing, so you should compare the process route for each layer before comparing manufacturing-time claims.
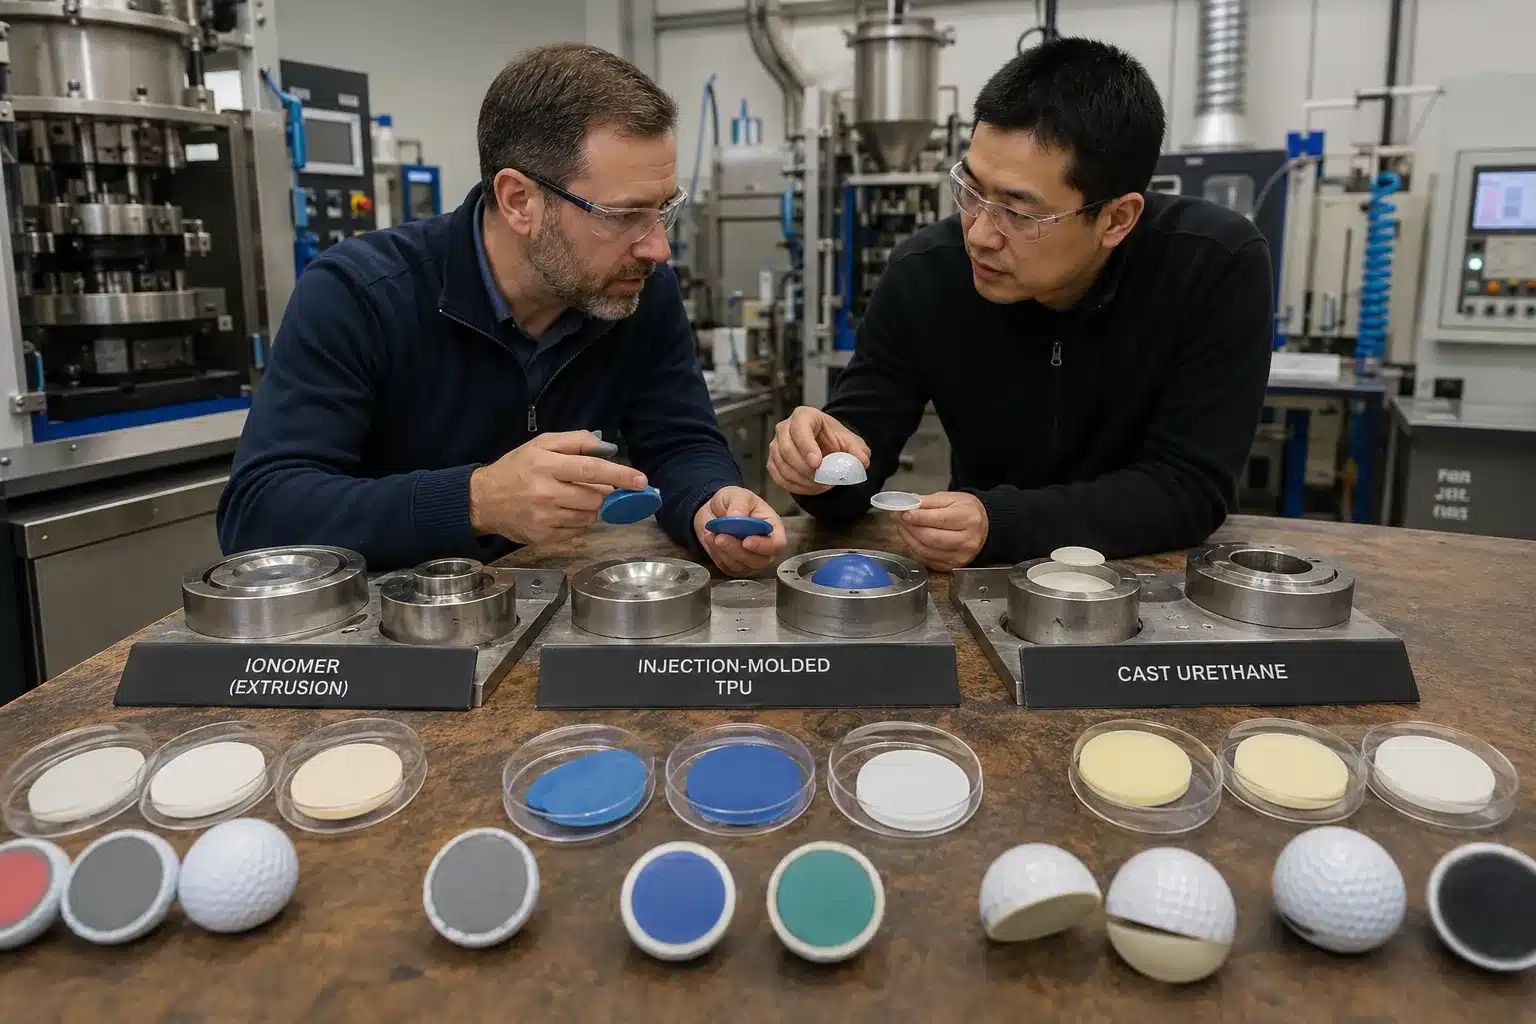
Injection TPU or Cast Thermoset Urethane?
The most useful purchasing rule is:
Process Route First → Layer Count Second.
| Pain / decision | Process route | Physical-time logic | Action / evidence |
|---|---|---|---|
| Standard cover | Ionomer / Surlyn | Thermoplastic forming and cooling | Confirm molding route |
| Urethane quote | Injection-molded TPU | Thermoplastic injection and cooling | Require TPU route declaration |
| Premium cast route | Cast thermoset urethane | Reaction, gel, cure, demold and finishing | Request cure and release stages |
| “3-piece vs 4-piece?” | Any construction | Layer count alone does not define time | Compare each layer’s route |
Surlyn and other ionomers belong to thermoplastic material families. Their manufacturing logic typically centers on controlled forming, cooling, demolding, and subsequent finishing.
TPU is also thermoplastic polyurethane. In many OEM golf ball programs, pelletized TPU is processed through injection molding; compression molding may also be used in some routes. Temperature, material flow, pressure, mold conditions, and cooling all influence the stage.
Cast thermoset urethane is different. Reactive liquid components are combined and cast around the ball subassembly. The material then depends on chemical reaction, gel and curing behavior before demolding, with subsequent finishing steps where required.
Technical golf ball TPU molding documentation makes the route distinction especially clear: thermoplastic polyurethane can be injection molded, while cast thermoset polyurethane contains physical gel and cure requirements before demolding and can require subsequent finishing.
The exact hours remain formula-, equipment-, and process-specific. A patent example is useful for understanding why two routes behave differently; it is not a universal stopwatch for every golf ball factory.
That is also why layer count is a poor standalone predictor of golf ball manufacturing time. A 3-piece cast-urethane ball can contain a chemistry-dependent stage that does not exist in the same form in a different multi-layer thermoplastic construction. Conversely, adding another molded layer adds its own processing but does not automatically prove that every 4-piece ball must take longer than every 3-piece ball.
“Urethane” quoted without a process-route declaration is a failure signal.
If your decision moves into feel, spin, pricing, MOQ, positioning, or performance differences, continue with the dedicated TPU vs cast urethane golf balls guide.
Use one verification request in your RFQ:
State the cover chemistry and forming route used for this SKU—ionomer injection, TPU injection or compression where applicable, or cast thermoset urethane—and provide the route-specific process traveler showing the required cooling, curing, finishing, and release stages.
Supplier shall identify the approved cover chemistry and forming route for the production SKU and keep that route consistent with the approved manufacturing reference. Any route change that affects molding, curing, finishing, coating, or release shall be disclosed before production continues.
✔ True — A 3-piece cast route can run on a different physical clock from a multi-layer thermoplastic route
Layer count matters, but material chemistry and forming method determine which physical processing stages the product actually needs.
✘ False — “Every 4-piece golf ball automatically takes longer to manufacture than every 3-piece golf ball”
Compare the process route first, especially cover chemistry and forming method, before using layer count as a timing shortcut.
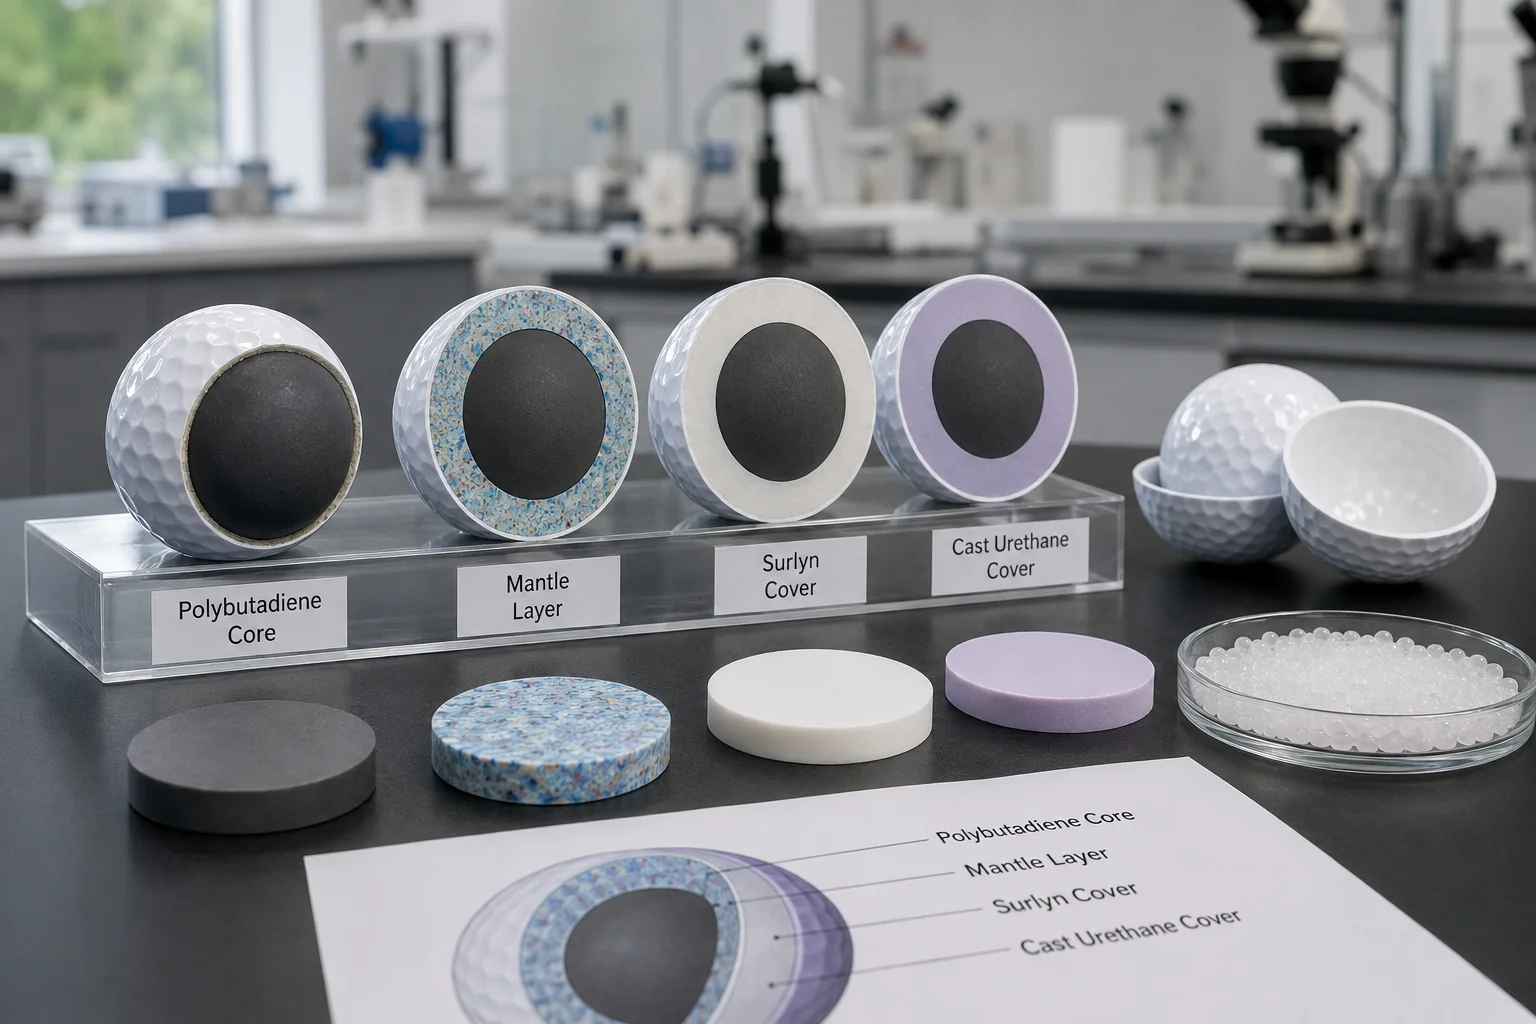
Which Time Drivers Cannot Be Compressed Safely?
When a launch is urgent, every day can look negotiable. The manufacturing route does not see every hour the same way.
Some manufacturing time is a scheduling variable; some is a process requirement. You may be able to reduce waiting or improve sequencing, but you should not assume that chemical curing, required cooling, coating release, inspection, or corrective work can be deleted simply because the order is urgent.
A useful distinction is Required Process Time Driver versus Corrective Manufacturing Delay.
Required process time exists because the product or batch has to reach and prove a controlled manufacturing state. Depending on the construction and route, this can include conditioning, cooling, chemical reaction, gel, curing, post-cure, coating drying or stabilization, and the inspection required before release.
Corrective manufacturing delay appears when the planned process does not pass as expected. A coating defect, printing nonconformity, out-of-window measurement, QC hold, segregation, remake, reinspection, or process correction can all extend batch elapsed time.
Those two categories deserve different buyer responses.
If a required material state has not been reached, the right question is whether the approved process gate has been satisfied—not how much a rush fee costs.
Public technical guidance on golf ball curing consistency illustrates why this matters. In a cast thermoset route, curing temperature and time affect material formation and cover durability. Too little or too much process time can create quality problems. That makes curing a manufacturing-control requirement rather than decorative waiting.
Cooling and coating release deserve the same discipline. If the next stage assumes the product has reached a specified physical condition, skipping that condition simply moves risk downstream.
Corrective manufacturing time is different. It exists because output must be contained, sorted, scrapped, remade, or checked again. That time is undesirable, but it can be doing something commercially useful: preventing known nonconforming product from becoming customer inventory.
If a supplier proposes a dramatically shorter physical route, treat it as a verification gap, not automatic evidence of dishonesty. Ask which stage changed, why the different route is appropriate for your SKU, and what release evidence remains.
Required curing, cooling, coating-release, and final-QC gates should not be bypassed solely to meet a requested date.
How Do Printing and Finishing Affect Batch Time?
A logo can appear on the ball in seconds, and a coating spray pass can look equally fast. Neither observation tells you when the full finishing stage closes.
Golfara normally reserves about two days for surface finishing, about two days for coating, and about one day for printing under a standard approved route. Those windows represent complete production stages—including preparation, application, curing or drying, handling, inspection, and release—not the speed of one spray or printing action.
For coating, Golfara does not release a batch just because the surface appears visually dry.
The practical release sequence is:
non-tacky → fully cured → adhesion check → color / gloss confirmation → release
That sequence explains why Application Time ≠ Finishing-Stage Time.
A spray operation itself may be quick. The coated balls still need to reach the approved condition and pass the checks that allow the batch into the next manufacturing stage.
If the surface remains tacky, curing is incomplete, adhesion fails the applicable check, or the color and gloss do not match the approved reference, the affected material cannot simply advance because the equipment has finished spraying.
Printing works the same way. Golfara’s approximately one-day standard production-printing stage can include setup against the approved artwork, repeated batch printing, applicable drying or curing, handling, visual inspection, and print-stage release.
The artwork shape also matters. A one-color logo in one position is not the same manufacturing task as multiple positions, several artwork versions, gradients, fine text, or difficult registration.
Pad printing generally suits repeated, simpler, lower-color work well. UV printing is useful for complex multicolor, gradient, or personalized designs. Neither is universally faster. Quantity, artwork complexity, color count, positions, sides, independent print actions, surface preparation, curing requirements, and inspection all influence the stage.
That distinction protects you from another weak shortcut: color count alone does not define printing time.
For detailed method selection, ink, adhesion, artwork feasibility, and durability, move to the dedicated golf ball printing methods guide.
Coated balls shall not advance to the next controlled manufacturing stage until the applicable surface is non-tacky, curing is complete under the approved process, adhesion passes the agreed check, and color and gloss match the approved reference.
✔ True — A coating stage can remain open after spraying stops
The batch may still require curing, stabilization, adhesion confirmation, reference matching, inspection, and formal stage release before it can move forward.
✘ False — “If the coating looks dry or the logo is already printed, the batch is ready for the next stage”
Visual completion and equipment completion are not the same as manufacturing release. Ask what conditions actually close the stage.
When Is a Golf Ball Batch Actually Finished?
Your production board can show the ordered quantity as completed while the batch is still sitting behind a QC hold. For the buyer, that difference defines whether manufacturing has actually ended.
A golf ball batch is not manufacturing-complete simply because molding, coating, or printing has stopped. If final QC places part of the batch on hold, the manufacturing clock can continue through segregation, scrap, remake, reinspection, and release before the order becomes a finished production batch.
What Happens When QC Stops Release?
Final manufacturing release can still depend on physical condition, weight, diameter, compression consistency, concentricity where relevant, coating condition, printing quality, visible defects, and disposition of nonconforming output.
This section is not about turning you into a quality engineer. It is about knowing whether the manufacturing clock has actually stopped.
| Pain / decision | Batch status | What still remains | Action / evidence |
|---|---|---|---|
| Balls are molded | In process | Finishing, coating, printing and QC | Continue routing |
| Printing is complete | Not necessarily released | Final inspection and disposition | Check QC status |
| QC finds nonconformance | Hold | Segregation and disposition | Record affected quantity |
| Replacement units are made | Pending release | Applicable reinspection | Verify corrected quantity |
| Final QC passes | Manufacturing released | No unresolved manufacturing gate | Record batch release |
Major-brand manufacturing provides a useful external benchmark for the same principle. Titleist’s Ball Plant 3 quality-assurance process states that production is halted when sampled output falls outside specification until the root cause is identified and corrected. A QC hold can therefore add manufacturing time because the process is containing and correcting risk rather than simply allowing suspect output to continue.
In August 2024, we were producing a 24,000-ball batch of 2-piece Surlyn golf balls when final QC identified a printing nonconformity affecting 982 balls. We traced the issue to a partially blocked ink supply line, rejected and scrapped all affected balls, and produced 1,200 replacements.
After the replacement quantity passed the required reinspection, the batch was released approximately two days later than originally planned. The original production quantity had already been completed, but the batch was not finished from a manufacturing-control perspective until the nonconforming units were contained, replaced, reinspected, and released.
A short equipment-level problem can therefore create a much larger batch-level time effect.
The ink-line issue itself did not consume two days simply because a component was blocked. The elapsed-time effect came from detecting the affected output, isolating it, scrapping the nonconforming balls, producing replacements, reinspecting them, and closing the batch release.
That is the distinction procurement teams need when a supplier tells them manufacturing is “done” but QC has not released the lot.
Production quantity treated as finished despite an unresolved QC hold is a failure signal.
If QC delays release, ask for the batch reference, hold reason, affected quantity, disposition, remake or rework quantity, reinspection status, and final manufacturing-release status. Those fields tell you whether the additional time is uncontrolled delay or a documented corrective action.
For the detailed test methods behind compression, dimensions, concentricity, durability, and other release gates, use the dedicated golf ball manufacturing quality control guide.
The endpoint here is simpler:
The batch is finished when every applicable manufacturing release gate is closed—not when the planned quantity has merely come off the equipment.
FAQ
Does new dimple tooling count as manufacturing time?
New dimple tooling can extend the overall project calendar, but tool development should normally be separated from the active golf ball manufacturing-process clock once the approved tool is ready for routine production.
A new tool may require design, machining, trial molding, inspection, correction, and approval before normal batch production begins. That work is real, but mixing it into one universal golf ball manufacturing number makes supplier comparisons less useful.
When comparing physical manufacturing time, confirm whether the quoted route assumes existing approved tooling or development work that has not yet been completed.
Should logo approval count as manufacturing time?
Buyer artwork approval normally belongs outside the physical manufacturing-process clock. After the artwork is approved and enters production, printing setup, batch printing, applicable drying or curing, inspection, and print-stage release become manufacturing activities.
This distinction prevents buyer waiting time from being blamed on the physical golf ball production process.
If an artwork file waits for approval, manage that through your OEM order schedule. Once the approved file enters printing, the factory-stage work belongs to manufacturing time.
Can packaging extend the order after balls are done?
Yes. Packaging can extend the overall OEM order schedule after the balls are manufacturing-complete, but custom boxes, sleeves, inserts, and carton production should not be presented as physical golf ball manufacturing process time.
Keep the two clocks separate.
The ball-manufacturing clock should focus on producing and releasing the golf balls themselves. Packaging may have its own production path and constraints, but those belong in packaging and OEM lead-time planning rather than this factory-process clock.
Why can two batches of the same SKU take different time?
Two batches can follow the same approved process route and still have different elapsed manufacturing times because stage handoffs, inspection findings, holds, replacement production, or corrective work can differ from one batch to another.
A slower second batch does not automatically mean the material formula changed.
First ask what happened inside the route: Did coating need correction? Was part of the batch held? Were replacement balls produced? Did an inspection gate require additional work?
The controlled process can remain the same while batch-level elapsed time changes.
What proves a coating stage is released?
A coating stage should use defined release conditions rather than “looks dry.” Golfara checks the applicable surface for non-tacky condition, full cure under the approved process, adhesion, and color and gloss agreement with the approved reference.
Those checks are why coating-stage time can continue after spray application has stopped.
Do not demand a universal number of curing hours across all formulas and factories. Ask what the approved process for your SKU requires and what evidence authorizes movement to the next stage.
Can replacement balls stay in the same batch?
Replacement balls can remain part of the corrected production order when the factory maintains the required batch reference, records the disposition of rejected units, identifies the replacement quantity, and completes the applicable reinspection before final release.
The important point is control.
Your records should show which quantity was rejected or scrapped, how many replacement balls were made, how those replacements were inspected, and whether the final corrected batch was released. Replacement production should not disappear inside a vague “quantity completed” status.
Conclusion
Golf ball manufacturing process time is best understood through Route → Stage → Release. Process route predicts the physical clock better than layer count alone, while machine speed tells you far less about customer batch completion than many capacity claims suggest.
At Golfara, many standard active-stage sequences total roughly 13–16 days. Current customer-facing production-planning references are intentionally wider—15–25 days for 2-piece Surlyn / ionomer, 18–30 days for 3-piece Surlyn / ionomer, and 30–50+ days for 4-piece cast thermoset urethane—because the routed process, finishing, QC, corrective work, and route-specific physical requirements still have to reach manufacturing release.
A molded ball is not necessarily finished. A printed ball is not necessarily finished. Even the full planned quantity is not necessarily finished if a manufacturing gate remains open.
The manufacturing clock tells you how the golf ball is physically produced and released; the OEM lead-time clock tells you when your order moves through the factory calendar. You need both numbers, but they should never be treated as the same number.
You might also like — China Golf Ball OEM Lead Time: What Controls the Schedule?