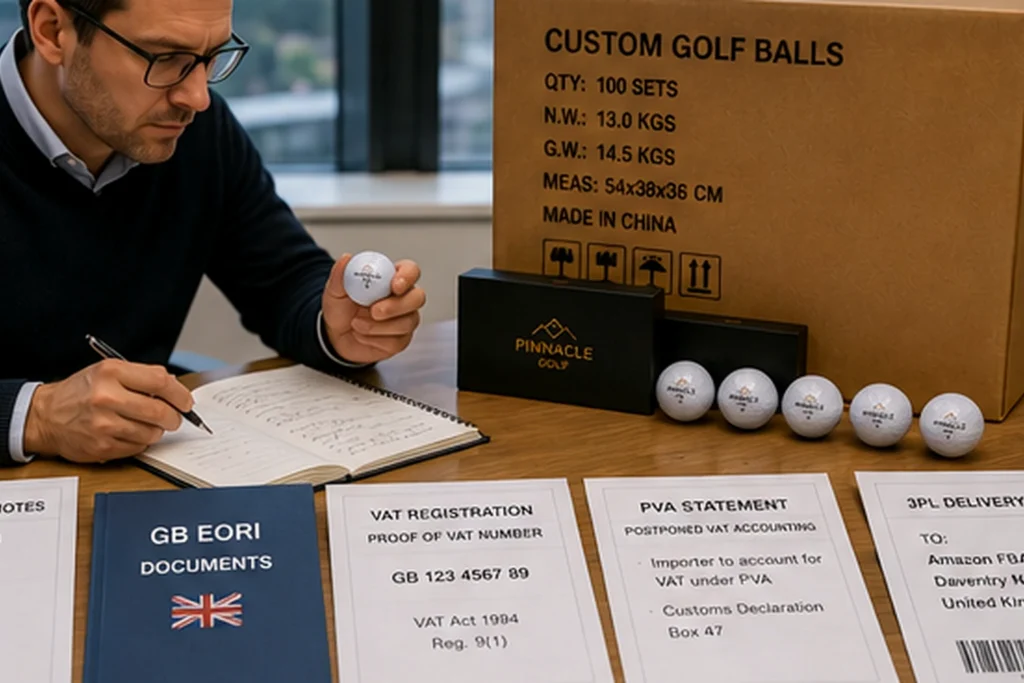
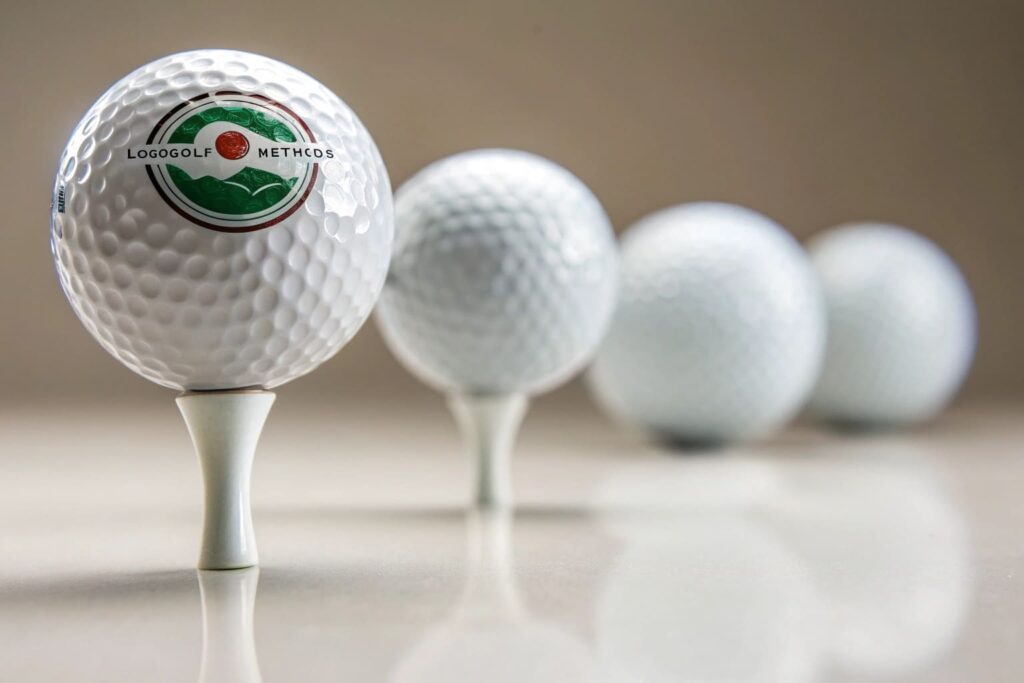
Your logo can look perfect on screen and still fail on the ball when small text, multiple colors, dimples, or a changed finish meet real production.
Choose a golf ball logo printing method from the artwork and final surface first. Pad printing may suit simple spot-color logos, while gradients, complex full-color detail, or variable personalization may require a digital route; either way, approve the result at actual print size on the exact ball and finish before mass production.
The method name is only part of the decision. Ask what the logo must reproduce clearly on the real ball, then lock the print route, physical proof, and production version your supplier must repeat.
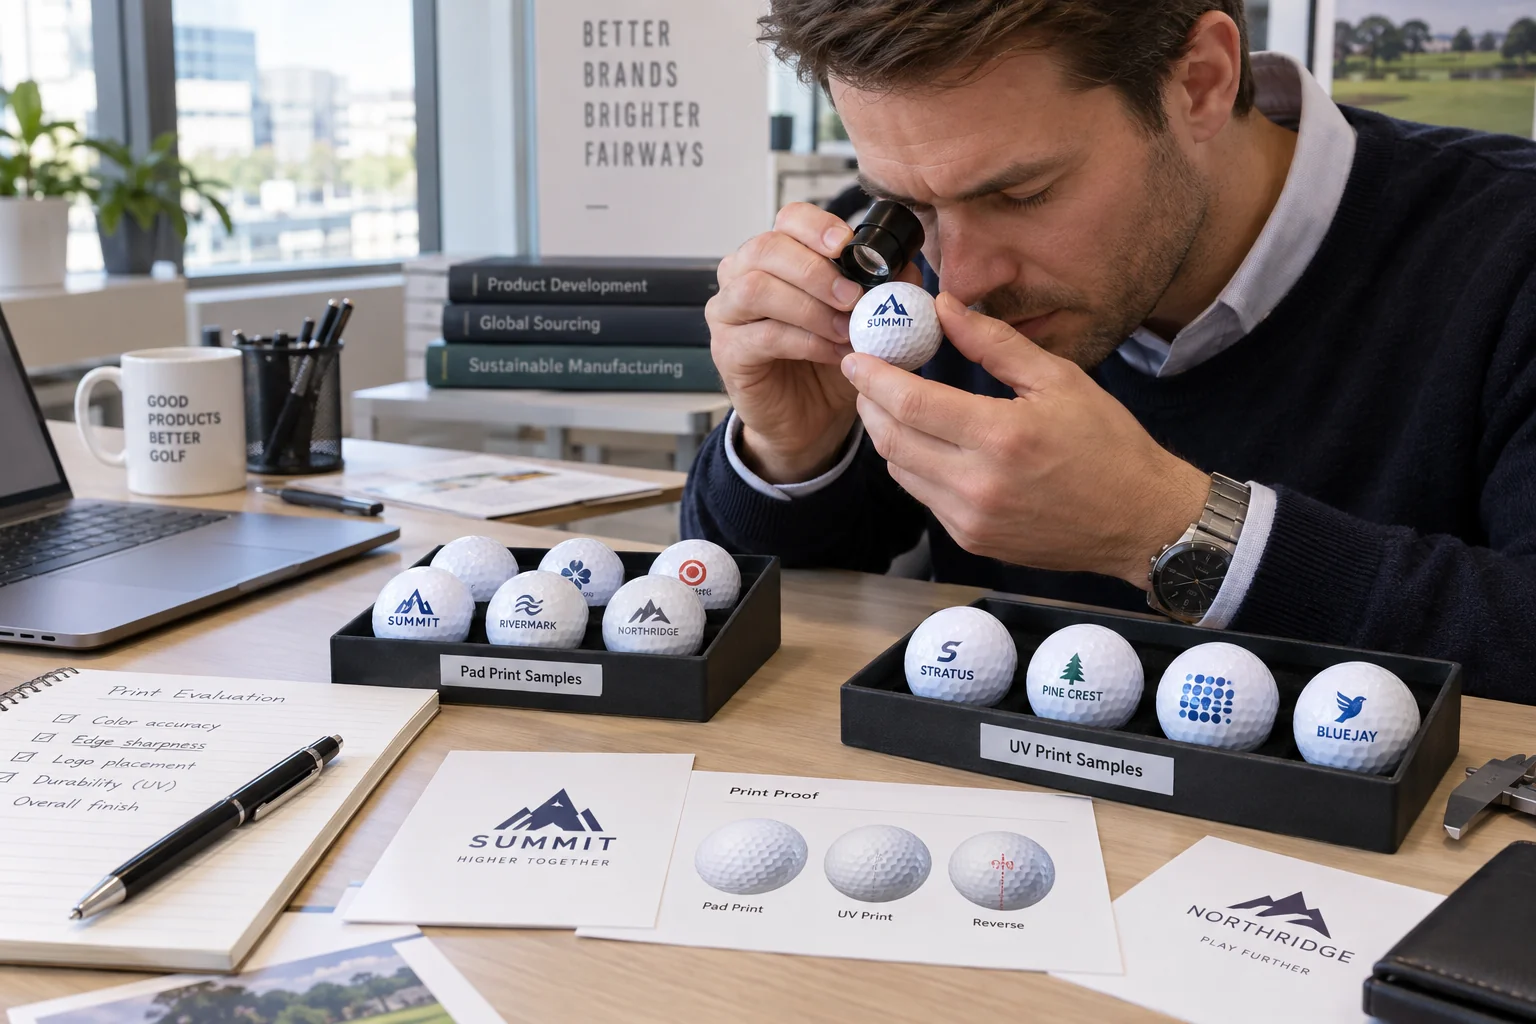
Which Printing Method Fits Your Artwork?
A supplier may recommend Pad or UV before checking your gradients, small text, print positions, registration demand, or actual production size.
Your artwork should choose the printing shortlist before process preference does. Simple solid-color logos may suit pad printing, while gradients, personalization, or complex full-color detail may require another route; approve the method only after the actual logo reproduces correctly on the final ball at intended size.
| Artwork decision | Possible route | What can fail | Evidence | Buyer action |
|---|---|---|---|---|
| 1–2 solid spot colors | Pad may be simpler | Unnecessary complexity | On-ball proof | Ask why Pad fits |
| Multiple spot colors | Pad or another route | Registration / stamp demand | Color-position map | Count print actions |
| Gradient / full color | Digital/UV may fit | Detail rendering | Physical proof | Name exact process |
| Micro-text / thin line | Proof decides | Edge breakup | Smallest-detail proof | Approve smallest element |
| Variable personalization | Digital may be practical | Version complexity | Personalized proof | Lock the route |
A more advanced-sounding technology is not automatically a better choice. Marabu’s golf-ball ink guidance lists golf-ball pad-printing systems, including a UV-curing pad ink, so “Pad versus UV” is not always a complete specification. Ask for the printing process, ink system, curing route, and exact substrate/finish.
How Many Pad-Printing Actions Does Your Logo Need?
On our current six-station Pad-printing setup, six stations are better understood as roughly six independent print actions, not simply six colors. One color in one position may use about one action; two colors in one position, or one color in two positions, may use about two. Multi-position, multi-color artwork can consume those actions quickly.
Before you approve a print route, it helps to see how golf ball logo printing is actually set up and checked in production.
A UK retailer came to us after a previous supplier had used pad printing for complex multi-color artwork. Fine edges were blurred and the retailer experienced returns. We reassessed the artwork, selected the UV printing route used for that project, and required the physical printed sample plus 20× macro edge photos before release. The buyer approved production only after reviewing the real result. The problem was not that pad printing was “bad”; it was the wrong route for that artwork.
A supplier recommending Pad or UV before reviewing the final artwork is a failure signal. Ask which artwork feature drove the recommendation; for multi-color or multi-position Pad work, request a simple color/position/stamp map.
You can write the production acceptance condition this way: Mass printing shall not be released until the buyer approves the logo on the final ball model and finish at intended print size, including the smallest text, thinnest line, placement, and required registration.
✔ True — The artwork and physical result decide whether the route fits.
A useful recommendation explains which requirement drove the process choice.
✘ False — “UV is automatically the premium choice.”
A technology name is not a quality grade. The simpler route can be better when it reproduces the approved artwork more reliably.
What File Makes a Logo Print-Ready?
A logo can stay razor-sharp at 500% zoom while critical text or lines become unreadable at the size actually printed on a golf ball.
A print-ready logo is not simply a high-resolution file. You need one controlled artwork revision that preserves required text, edges, spacing, and color structure at actual golf-ball print size, because even perfect vector artwork can contain details that are physically too small to reproduce reliably.
Current Titleist custom-logo requirements accept vector and raster formats and use a digital proof before production. That supports a file → proof → approval workflow, but it does not make a digital proof sufficient for OEM physical release.
Your Artwork Requirement Brief should lock the revision, intended width and height, color structure, smallest critical detail, thinnest line, and print position. If a buyer sends several logo versions through email or chat, one file should be explicitly designated as the production revision before sampling begins. Otherwise a correct sample can still be made from the wrong artwork version.
On our current Pad-printing setup, useful working windows are about 20 mm diameter for round artwork, 18 × 18 mm for square artwork, 22 mm wide for horizontal artwork, 25 mm high for vertical artwork, and up to about 29–29.5 mm high for some narrow designs at 4 mm width or less. These are our working ranges, not universal standards.
For example, two 16 mm logos separated by 6 mm create about 38 mm total width. The station count may be manageable, but the layout exceeds our normal horizontal Pad-printing window of about 22 mm. The constraint is print area, not station count.
Putting alignment lines and sidestamps must also fit the actual print area. On our current pad-printing setup, some narrow designs no more than 4 mm wide can reach approximately 29–29.5 mm in height. However, this is a working reference, not a guaranteed limit for every line, orientation, or position. A primary pole logo and a separate side alignment mark may require different print actions, depending on the approved artwork and equipment setup.
A continuous 360° wraparound alignment stripe presents additional production challenges. For our current pad-printing approach, we generally recommend limiting wraparound designs to one or two colors to reduce rotational registration errors, visible joins, and alignment inconsistencies. Six available printing stations do not eliminate these constraints. Confirm the production route and inspect a fully printed physical sample before approving mass production.
That is why the smallest text, thinnest line, reversed detail, ® or ™ mark, and negative space deserve more attention than the largest part of the logo. Approve those critical elements at actual size before production proofing.
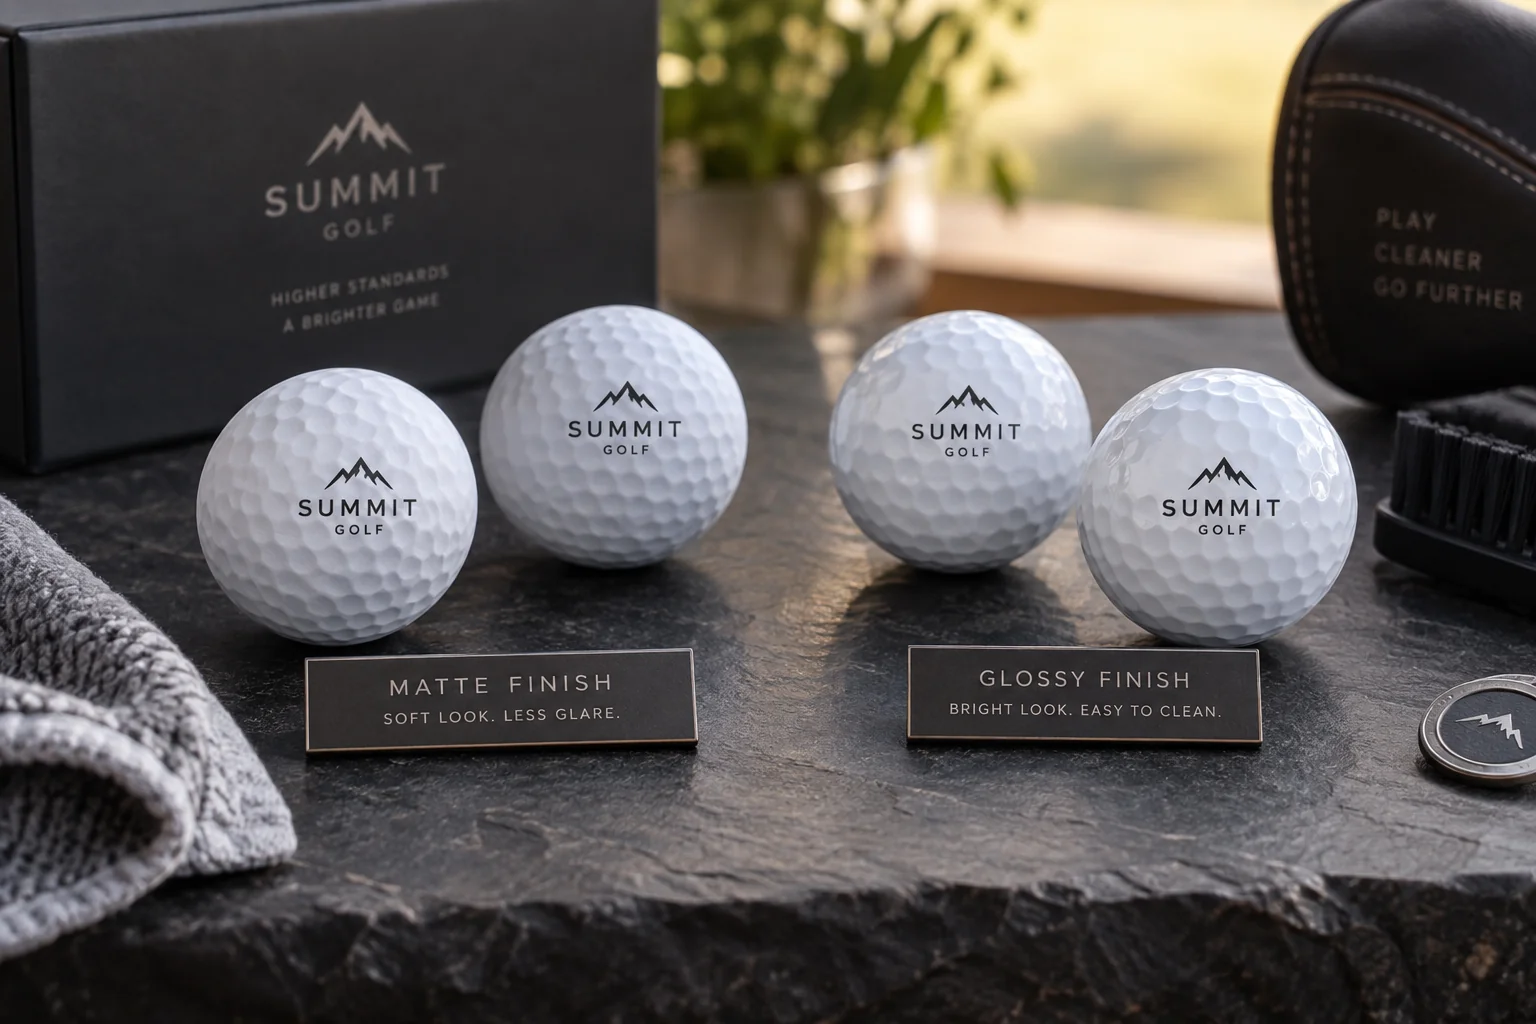
Does Matte or Glossy Change the Print Choice?
A glossy proof can become the wrong reference when the production SKU is switched to matte because the render appears more premium.
Matte and glossy custom golf balls can use the same artwork, but the finish should remain part of the approved print version. matte can change surface condition, appearance, handling, and production complexity, so your safest approval is the actual logo printed on the exact finish you will mass-produce.
We manufacture custom-logo golf balls in both matte and glossy finishes. In our programs, matte typically costs more than the equivalent glossy finish on the same ball platform because it can add coating-material requirements, coating or curing work, yield control, finish-specific QC, and line cleaning or changeover. That is our manufacturing experience, not a universal market rule.
Matte has lower reflected gloss and a drier, frosted hand feel that some premium-positioned programs prefer. In our handling experience, especially on white balls, matte surfaces can show or retain dust, grass residue, mud, and water marks more readily than a smoother glossy finish. In the same handling checks, we generally find the smoother glossy finish easier to wipe clean.
That matters commercially. A matte finish may look excellent in a corporate-gift presentation but create a different appearance-aging expectation in a simulator, academy, range, or other high-handling program. If your team is undecided, compare physical matte and glossy samples after normal handling instead of choosing from a clean render.
One granted U.S. golf-ball patent illustrates a matte manufacturing route involving a dedicated matting-agent formulation, pretreatment, top coating, and curing. That supports one practical point: matte can represent a different production condition, not just a lower-gloss appearance. It does not mean every factory uses the same matte process or charges the same premium.
Do not assume that a rougher matte surface automatically creates more spin or stopping power. That would require controlled comparison testing on otherwise matched golf balls.
For sourcing, the practical rule is simpler: do not use a generic glossy sample to approve a matte production order. If the finish is still undecided, request both physical versions and compare print appearance, feel, and cleanability.
For version control, you can write this into the PO:
Supplier shall identify the approved print version by artwork revision, ball model, final cover/finish, print method, and physical proof sample ID. Any material change to these items shall require written re-approval before mass printing.
✔ True — Finish is part of the physical production condition.
If glossy becomes matte, confirm that the approved print still represents the surface and appearance the customer will receive.
✘ False — “Matte is only a cosmetic change that can be made after proof approval.”
A finish change can alter the coating system and printed surface, so it can trigger re-proof.
Can You Print on Urethane Golf Balls?
A clean logo on another golf ball can prove capability while telling you little about compatibility with the urethane SKU you plan to buy.
Yes, you can print on urethane golf balls, but a successful print on another cover does not automatically approve your urethane SKU. Require physical proof on the actual ball model and final finish before releasing that print version for production.
Treat this as capability versus compatibility. Different surfaces and coatings can require different process conditions, so the controlled route should identify the printing process, ink system where relevant, curing route, and exact cover/coating/finish.
A supplier showing you a clean generic sample proves that it can print a golf ball. Your purchasing question is narrower: Can it reproduce your approved artwork on your exact SKU and finish?
Request the final on-ball proof on the ordered SKU. If you are still choosing the cover family itself, use the Surlyn vs Urethane OEM cover guide rather than turning print approval into a cover-selection exercise.
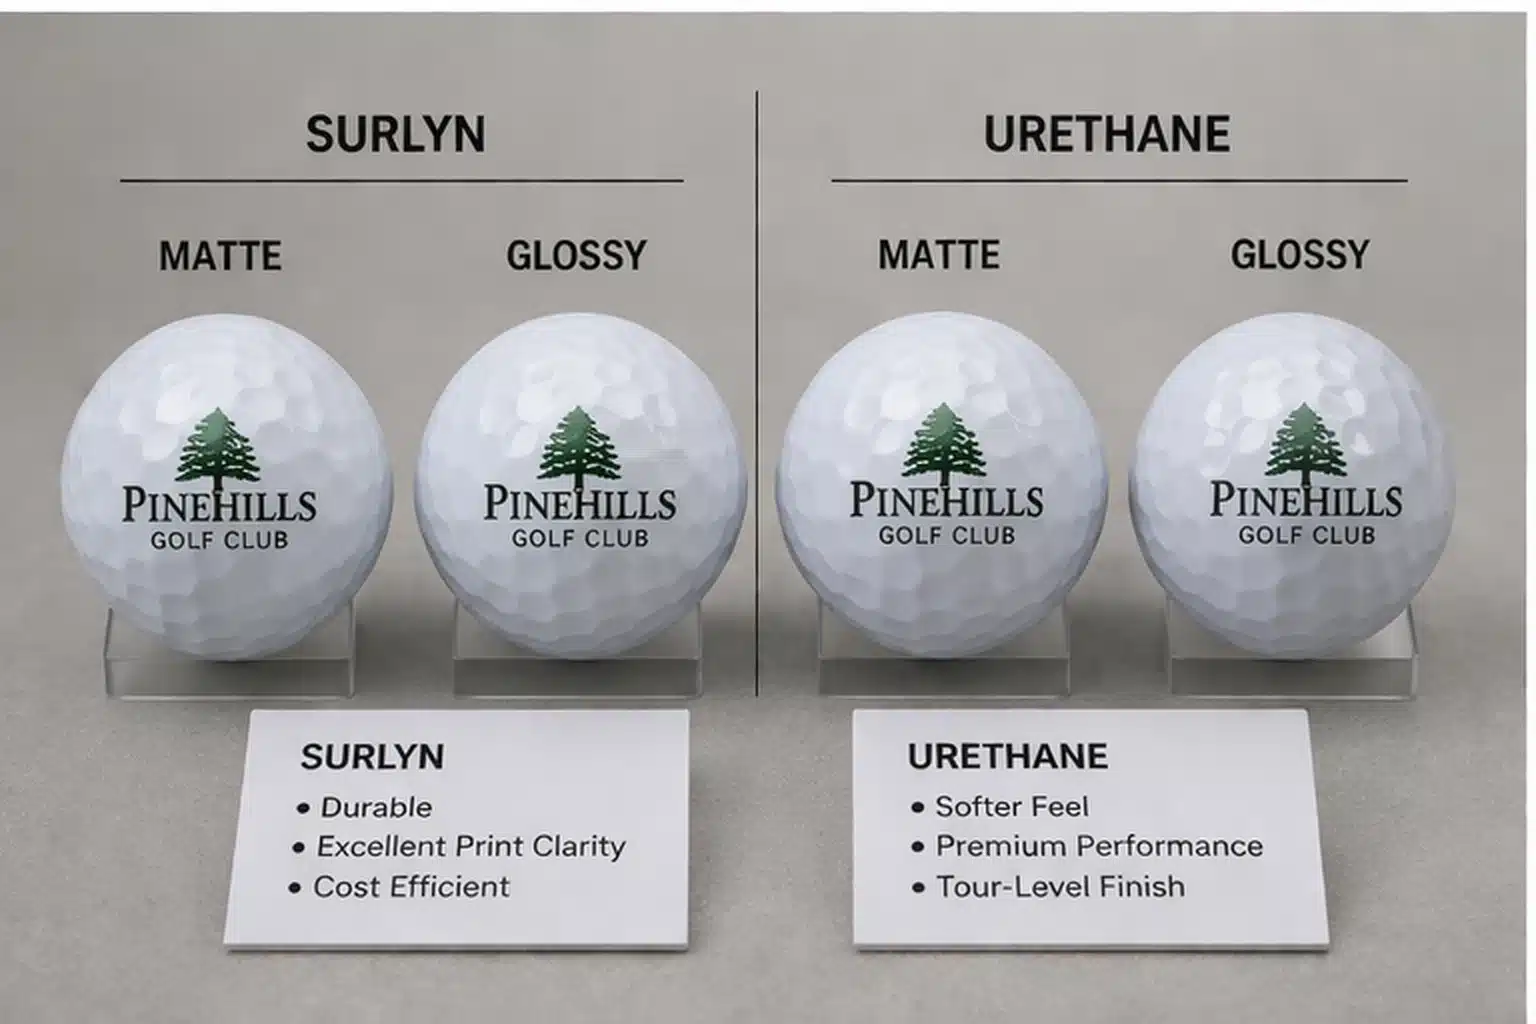
Can Printing Change Ball Performance?
It is easy to assume either that a logo can never matter or that adding more protective coating must automatically make the printed ball safer.
A normal logo should not be treated as a performance upgrade or penalty by assumption. Your buyer concern is process control: if the printing system, finish, or protective build changes materially, approve the finished version again rather than assuming a method name or heavier coating is automatically harmless.
Use case determines the next evidence gate. Corporate gifts may emphasize presentation; playable promotional balls add club impact; range and simulator programs add repeated handling, cleaning, and wear.
Record the intended application in a short Use-Case Note. Method selection belongs here; rub, hit, wipe, washer, peeling, and real-use wear verification belong in the guide to why custom golf ball logos wear off.
What Proof Should Release Mass Printing?
The artwork can be correct and the digital proof approved while production still lacks one controlled physical reference that everyone must repeat.
Do not release mass printing from artwork approval alone. Your release file should tie the approved artwork revision, actual print size, final ball model and finish, print route, and physical sample to one controlled version so production has a clear reference and your team knows what triggers re-approval.
| Release decision | What to lock | Evidence | If changed | Buyer action |
|---|---|---|---|---|
| Artwork | Revision + actual size | Final artwork | Re-proof | Stop old version |
| Ball surface | SKU + cover + finish | Physical sample | Re-proof | Approve exact SKU |
| Print route | Process + controlled system | Process record | Review / re-proof | Confirm route |
| Physical result | Placement + smallest detail | Sample ID | Re-proof | Lock reference |
| Production release | Approved-version status | Release record | Hold | Release matching version |
What Belongs in the Print Release Pack?
Keep the buyer-facing bundle compact: Artwork revision + Ball SKU + Finish + Print route + Physical proof sample ID + Approval record + Re-proof trigger.
A digital proof verifies layout intent. A physical on-ball proof verifies whether that artwork can actually be reproduced on the selected finished ball. They answer different approval questions.
For a ball combining a brand logo with a putting alignment line, review the actual printed sample from the golfer’s putting address position, not only in a digital preview or product photograph. Check whether the alignment line appears straight and clearly visible, whether the contrast is sufficient, and whether its position works with the main brand mark when the ball is placed for a putt.
If one bulk order includes different alignment-line colors, such as black and blue, record each colorway as a separate commercial Print Version. Identify the approved artwork, physical sample reference, quantity, and packaging requirements for each version. Confirm whether different printing setups or additional print actions are required rather than assuming that one approval covers every colorway.
Separate commercial Print Versions do not automatically create separate USGA/R&A conforming ball types. If an alignment line or sidestamp may affect the ball’s official identification markings, verify the applicable requirements in our private-label USGA/R&A submission guide before finalizing production artwork.
Even after the physical proof is approved, the production lot still has to match that reference before shipment.
In one 24,000-ball two-piece Surlyn production lot, our final inspection found 982 printing nonconformities before shipment release after a partial blockage in the ink-supply line caused unstable ink delivery. We scrapped the affected balls, remade 1,200 replacements, and reinspected them before release. That correction added about two production days in this specific case.
Printing was complete, but the lot was not ready for shipment. The case is not a benchmark defect rate; it shows why production completion, inspection acceptance, and shipment release are separate control points.
Your Print Version Record should give the buyer, production team, and QC team one shared reference: the approved artwork revision, ball SKU, finish, print route, and physical sample ID.
For an OEM order that depends on actual size, finish, and surface appearance, a PDF alone should not be the final production reference.
Please confirm the proposed print method and provide the final artwork revision, intended print dimensions, ball model, cover/finish, physical on-ball proof, and approved sample ID before mass printing.
For broader batch inspection and lot-release controls beyond this print-version approval, use the guide on how to verify batch-linked golf ball QC evidence.
✔ True — Artwork approval and physical production-version approval are different gates.
The release record should connect the file, actual ball, finish, route, physical sample, and re-proof conditions.
✘ False — “Approving the artwork means production printing is approved.”
A correct file can still produce the wrong physical result. Mass printing needs a version-linked on-ball reference.
FAQ
Is Pad Printing Always More Durable Than UV Printing?
No. A process name alone does not establish durability because the result also depends on the ink system, curing route, surface, finish, and use case.
Choose the route from artwork and physical execution first. Verify real-use wear separately when durability matters commercially.
How Long Should a Printed Golf Ball Logo Last?
There is no universal lifespan for every ball, ink system, finish, and use case. Gift balls, playable promotional balls, and facility balls face different wear conditions.
Avoid fixed “X hits” claims unless the test is documented. Use dedicated durability evidence when lifespan is a purchasing requirement.
Can I Reuse the Previous Print Proof for a Reorder?
Only when the approved Print Version remains materially unchanged. The same logo file does not prove that the ball SKU, finish, placement, or route stayed the same.
Compare the previous record with the new PO and re-proof when a material production variable changes.
What If the Ink or Curing System Changes After Approval?
A change to the ink system or curing route should trigger a review of the approved Print Version, even if the artwork and printing process name stay the same. Confirm whether the previous physical proof still represents the production condition; if not, re-proof the changed system before release.
-
Compare the new ink/cure system with the approved record.
-
Keep the artwork revision and ball SKU identifiable.
-
Re-proof when the physical production condition no longer matches the approved sample.
Can One Approval Cover Logos on Both Sides of the Ball?
Only when both positions are represented in the approved artwork and physical sample. A front logo approval should not silently become approval for a second position with different placement, orientation, or registration requirements.
-
Define both print positions.
-
Lock orientation where it matters.
-
Confirm both sides on the physical production reference.
Can a Sample Photo Replace a Physical On-Ball Proof?
A photo can document appearance, but it does not always replace the physical proof needed for an OEM release decision. If actual size, finish, surface texture, placement, or handling appearance matters to your program, define whether the buyer must review the physical sample before release.
-
Use photos for documentation.
-
Use the physical sample when the surface itself affects approval.
-
Tie either form of evidence to the same artwork and sample ID.
Conclusion
Choose the print route from the artwork, approve it on the actual finished ball, and lock the physical version production must repeat. Pad or UV is only part of the decision; the buyer-safe result comes from matching artwork, actual size, final surface, process route, and physical proof before mass printing.
Use the decision chain:
Artwork Requirement → Actual Print Size → Final Surface → Print Method → Physical On-Ball Proof → Print Version Lock
You might also like — Why Is Your Custom Golf Ball Logo Wearing Off?