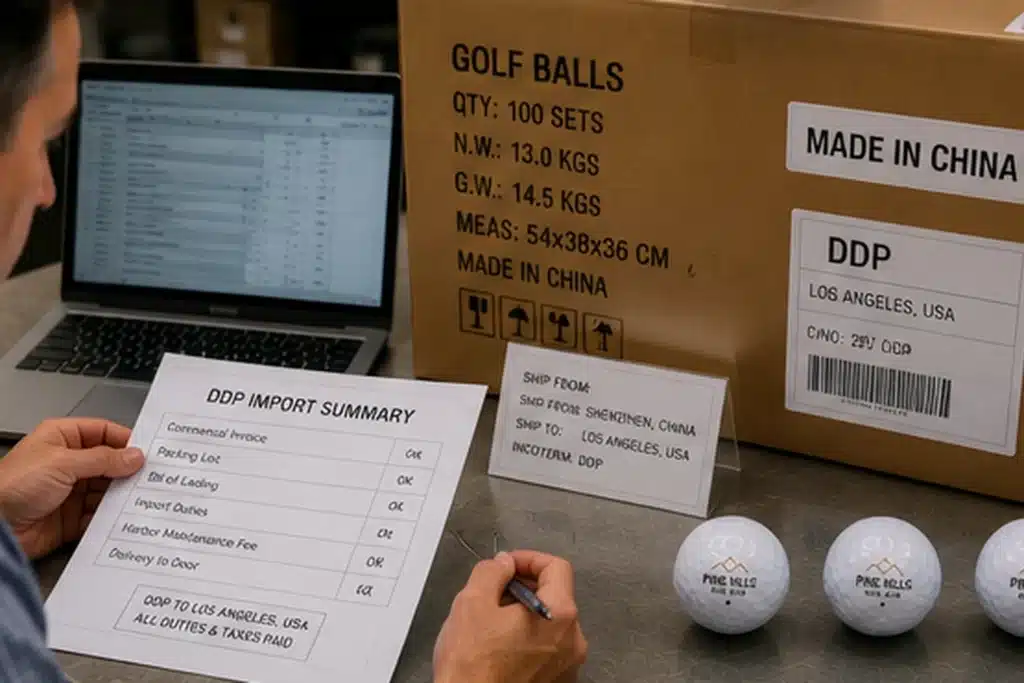
Yes—a 1,000–3,000-piece golf ball OEM trial can be realistic, but only when it uses a proven production platform, represents the SKU you intend to scale, freezes the approved specification, and leaves batch-linked evidence for the reorder. Factory acceptance alone does not make it a valid OEM pilot.
A factory may accept your 1,500-ball first production order and still use a substitute construction, temporary tooling setup, finish, or production route that will not carry forward to the next PO. In that case, you have a small accepted order—not a reliable manufacturing reference.
For low-volume golf ball OEM programs, use three tests: Reuse → Freeze → Prove. Reuse the intended production platform where possible, freeze the product and process references before production, and preserve evidence that lets the reorder be compared against the pilot.
Your first PO should therefore answer one practical question: Can this batch become the controlled production reference for the product you intend to scale? If the answer is no, a lower golf ball OEM MOQ has not necessarily reduced your sourcing risk.
Is a 1,000–3,000-Piece OEM Trial Valid?
A low golf ball OEM MOQ sounds useful until the second PO requires a different construction, tool, finish, or production route. Then the first run may have tested very little.
A 1,000–3,000-piece order is a valid OEM pilot only if it represents the product and production route you intend to scale. Your supplier accepting the quantity proves commercial willingness; it does not prove that the same construction, tooling, process reference, and QC baseline can support your next PO.
| Buyer decision | Accepted small order | Valid OEM pilot | Main risk | Buyer action |
|---|---|---|---|---|
| Product route | Can be temporary | Represents intended route | Wrong test | Confirm route |
| Construction | May be substitute | Represents final SKU | False market signal | Match product promise |
| Tooling | May be workaround | Reusable reference | Reorder reset | Record tool reference |
| QC | May only say pass | Batch-linked evidence | No comparison base | Request evidence |
| Reorder | Undefined | Same reference planned | Start over | Confirm reorder route |
Accepted Order or Valid Pilot?
The practical difference is whether your first PO leaves a reference that still matters on the second. A valid golf ball OEM pilot should use an intended, repeatable route rather than a one-off workaround created only to hit a small quantity.
For suitable programs, Golfara can support low-volume production in the 1,000–3,000-piece range when an existing construction, proven formula/specification, existing tooling, and mature finish can be reused. That is a supplier-specific capability, not a universal private label golf ball MOQ.
A setup fee may improve small-run economics, but it cannot create missing tooling, solve an incompatible route, or guarantee production capacity. A factory that accepts the quantity but cannot state whether your reorder will use the same route is a failure signal.
Request a written production-route declaration covering construction, specification reference, tooling, finish, and intended reorder route. If your issue is instead whether the ball, printing, or packaging minimum controls the order, first identify which MOQ is binding.
Supplier shall confirm whether the planned reorder can reference the same approved production route used for the pilot.
✔ True — A factory can legitimately accept a 1,000–3,000-piece production order
That order becomes a useful OEM pilot when it represents the intended SKU and leaves a reusable production reference.
✘ False — “Factory acceptance alone proves I have a valid OEM pilot”
If the intended product or manufacturing route must change materially for the reorder, the first order may be small without being a useful manufacturing pilot.
What Should Your First OEM Pilot Prove?
Trying to validate product performance, branding, packaging, supplier capability, channel demand, and every future customization in one first PO makes the result difficult to interpret. If too many variables change at once, your team may not know what the pilot actually proved.
Your first OEM pilot should answer two separate questions: will the market accept this product, and can the supplier reproduce the approved product route? A low-MOQ pilot loses value when you simplify the core construction so aggressively that the test no longer represents the SKU your customers will eventually buy.
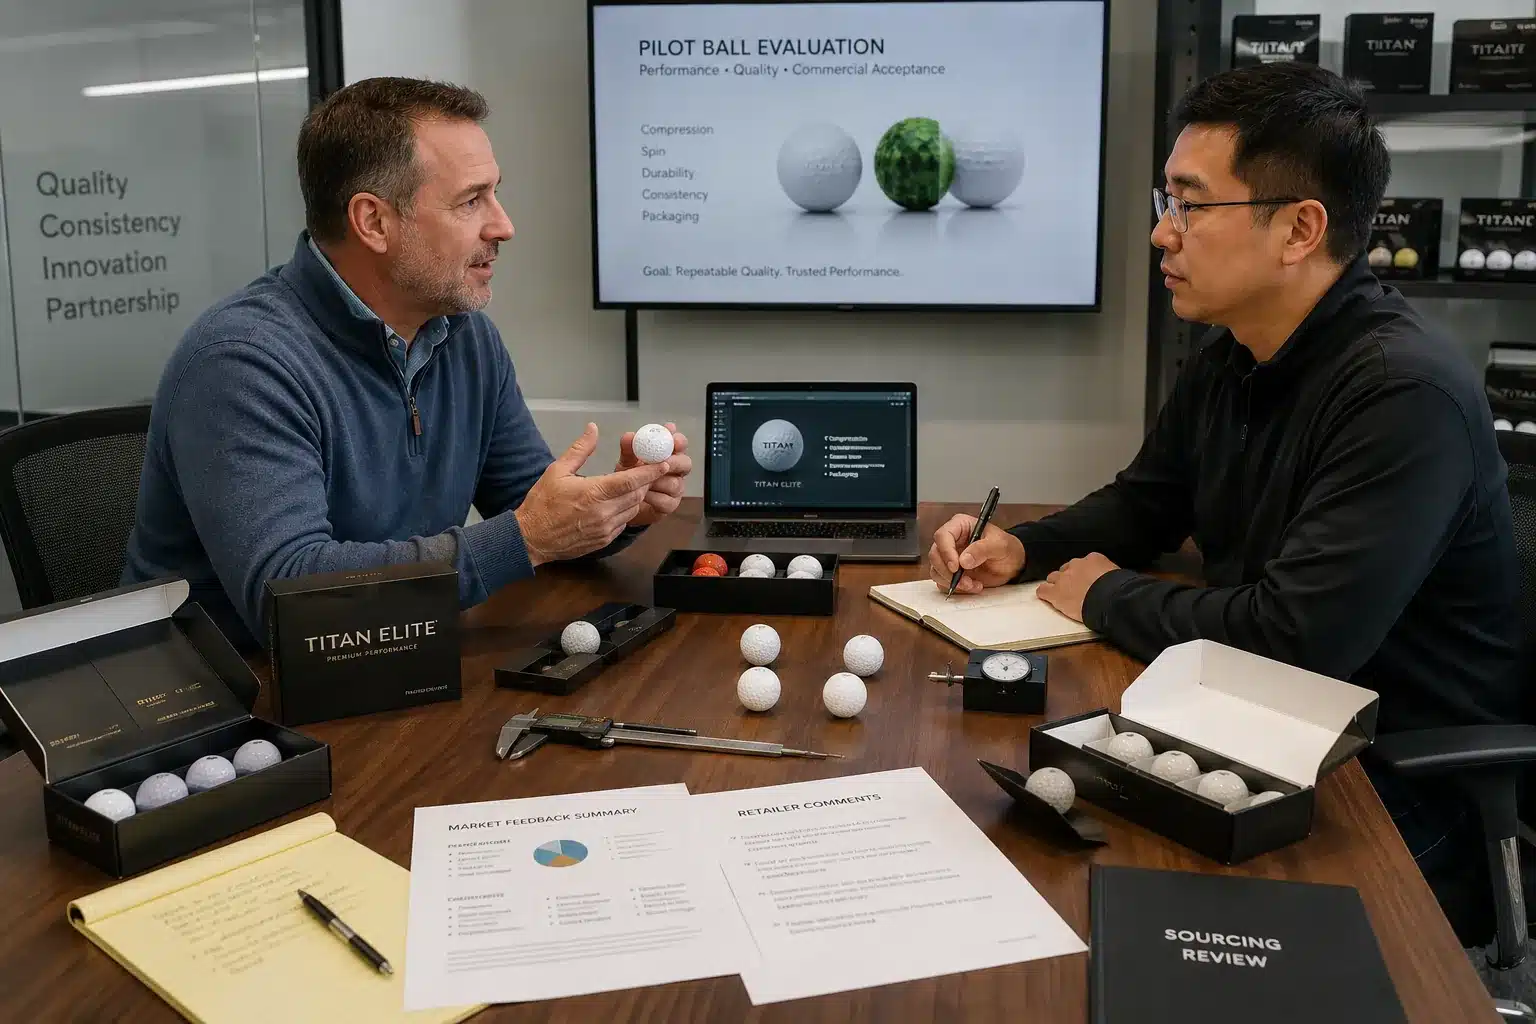
Your first PO should answer a market question, not solve every branding dream. But simplification has a limit: do not test the wrong product just to get a lower MOQ.
| Decision | Market Gate | Manufacturing Gate | Failure signal | Buyer action |
|---|---|---|---|---|
| Product | Customer accepts promise | Route matches intended SKU | Wrong construction | Match intended SKU |
| Branding | Logo/position accepted | Reference reproducible | Artwork drift | Freeze artwork |
| Packaging | Channel accepts pack | Route remains usable | Pilot-only workaround | Confirm pack route |
| Quality | Complaints acceptable | Evidence comparable | “QC Passed” only | Keep evidence |
| Reorder | Real demand appears | Same reference reusable | New route required | Hold scale |
Market Gate or Manufacturing Gate?
The Market Gate asks whether the product deserves another PO. The Manufacturing Gate asks whether the next PO can reproduce what the market just approved.
Use actual commercial evidence for the Market Gate: sell-through, distributor feedback, complaint records, realized margin, channel fit, and genuine reorder interest. Set those criteria before launch rather than choosing them after seeing the result.
For the Manufacturing Gate, confirm that the pilot used the intended production route, matched the approved reference, generated batch-linked evidence, and left a retained sample and reorder reference.
Product representation is where many low-MOQ pilot programs fail. A smaller order has little validation value if the ball you test does not represent the product your customers will eventually receive.
If your intended SKU is a premium 3-piece urethane ball, a fundamentally different 2-piece value ball may be easier to source at low quantity, but it validates a different product promise.
Use the simplest proven construction that still represents your intended SKU, target player, channel, and performance proposition. Require a short pilot-objective statement before sample approval. If the proposed construction changes the core product promise solely to reach a smaller minimum, reject the pilot design.
Can You Reuse the Intended Production Platform?
A 1,000-ball OEM trial becomes much harder to justify when the same first PO requires a new construction, new tooling, new formula, different cover route, and a new performance target.
A realistic low-volume OEM pilot usually reuses the production platform you intend to scale. Existing construction, formula, tooling, and finish reduce development variables; a new mold, formula, cover route, or performance target can move your project from pilot production into new product development.
Existing Platform or New Development?
Classify the manufacturing route before negotiating the pilot quantity. If the core route must first be created or redeveloped, the project is no longer only a small-batch production decision.
| Buyer request | Existing-platform pilot | New development signal | Main risk | Buyer action |
|---|---|---|---|---|
| Construction | Proven model | New architecture | Wrong scope | Classify route |
| Compression | Existing model | New target needs redevelopment | Formula change | Confirm option |
| Mold/dimple | Existing tool | New tooling | Validation burden | Record tool ID |
| Cover route | Mature process | Different process | Scale mismatch | Confirm route |
| Finish/color | Standard finish | New body-color route | Development work | Reclassify |
| Packaging | Proven route | New custom route | Separate constraint | Verify path |
An existing-platform pilot can still support a differentiated private-label product. It simply begins with a construction and production route the factory already understands instead of asking the first PO to carry unnecessary development risk.
At Golfara, we manufacture golf balls for both low-volume custom programs and larger production runs. From that experience, we have seen that factory size alone does not determine whether a supplier is well suited to a small-batch pilot.
A flexible manufacturer may be a better fit for the first production run when its production planning, line allocation, and order mix are structured to handle smaller programs efficiently.
Different cover routes can represent materially different manufacturing paths. For example, injection-molded TPU and cast thermoset urethane may both be described as urethane-covered golf balls, but they are not the same production route.
For your pilot, the purchasing question is simple: will the first production run use the same intended manufacturing route when you scale?
Custom compression follows the same logic. An existing factory model can remain an existing-platform choice; a target that forces formula or process redevelopment is development. A new body-color route can also move the project outside a mature platform; detailed color economics belong in the custom-colored golf ball MOQ guide.
Request an existing-platform declaration listing every proven construction, specification, tooling, finish, and process element, plus every feature requiring new development. If you are unsure who actually controls those production decisions, verify a China golf ball OEM supplier before relying on a pilot promise.
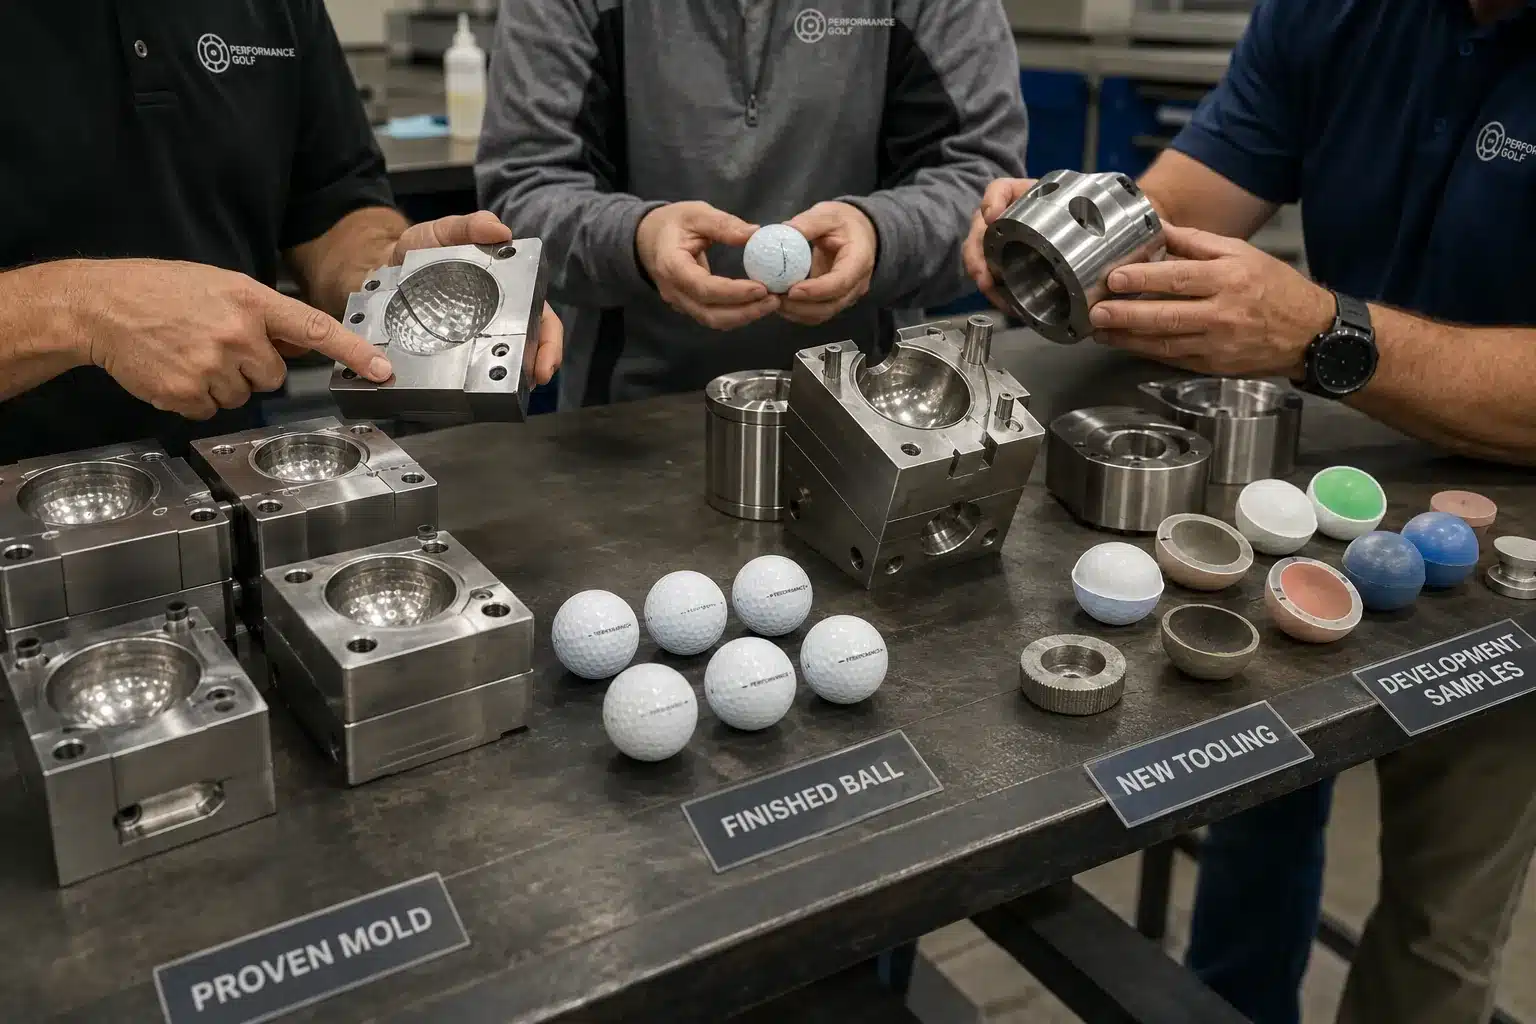
✔ True — Reusing a proven platform can make a small OEM pilot more realistic
You reduce development variables without automatically changing the product promise your market is supposed to evaluate.
✘ False — “Every custom specification change automatically raises ball MOQ”
Some changes affect cost, approval work, or timing. The project becomes new development when it requires a genuinely new product or manufacturing route.
What Must You Freeze Before Pilot Production?
A sample can look excellent and still become a weak production reference if construction, tooling, finish, artwork, packaging, or QC methods continue moving after approval.
Freeze the variables that define what your pilot is supposed to reproduce before production starts. Your construction, specification revision, tooling reference, finish, artwork, packaging route, approved sample, and QC method should not drift silently during the run, or the pilot loses value as a reference for the reorder.
Spec Freeze does not mean nothing can change. It means a change becomes visible, documented, and approved before it contaminates the comparison.
Before releasing golf ball trial production, freeze:
-
product construction and approved specification revision;
-
mold/tool and dimple/tool reference where applicable;
-
cover/process route and finish where relevant;
-
logo artwork revision, print positions, and sides;
-
packaging route;
-
approved sample ID;
-
QC method reference;
-
change-notification and buyer-reapproval trigger.
“Simple logo” is not synonymous with “one color.” Positions, sides, gradients, fine text, artwork versions, independent print actions, and registration difficulty can affect setup and approval work without automatically changing ball MOQ. Keep the deeper engineering in the custom golf ball printing methods guide.
If packaging becomes its own design decision, move that work to the OEM golf ball packaging guide.
A controlled-reference approach is consistent with ISO guidance on documented information for quality management systems. Specifications, inspection plans, measurement records, approved changes, and retained evidence help establish what was authorized and what was actually produced.
Request a pilot-production reference sheet carrying the specification Revision ID, approved sample ID, tooling reference, artwork revision, packaging route, QC method reference, and reapproval trigger. If the issue becomes why the bulk lot does not resemble the approved sample, use the dedicated guide to sample-to-bulk golf ball consistency.
Any material change to the controlled reference shall require written buyer notification and reapproval before production continues.
What Evidence Makes the Pilot Repeatable?
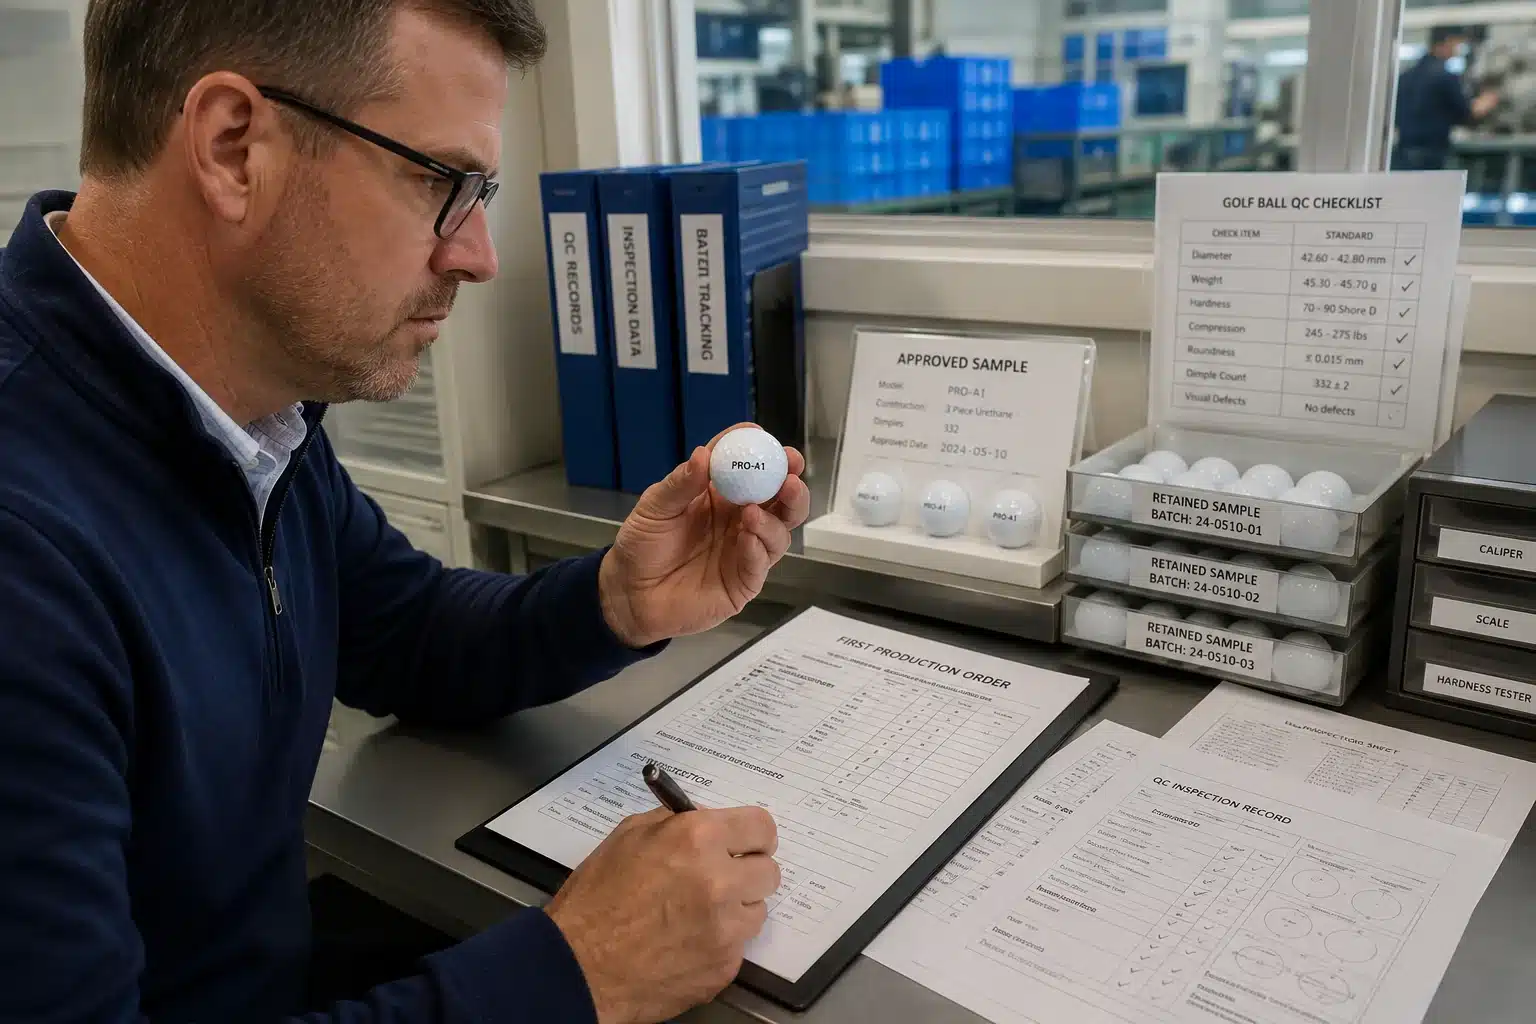
A polished sample and a one-line “QC Passed” report can leave your team with no defensible way to compare the pilot with the second production lot.
“QC Passed” is not enough evidence for a repeatable OEM pilot. Your pilot file should link the approved sample, specification revision, batch ID, individual QC results, test method, retained sample, and reorder reference so the next lot can be compared against the same controlled baseline.
Sample → Pilot → Reorder Evidence Chain
Treat the evidence as one chain: Approved Sample ID → Approved Spec Revision → Pilot Production Reference → Pilot Batch ID → Pilot QC Evidence → Retained Sample ID → Reorder Reference → Change Record.
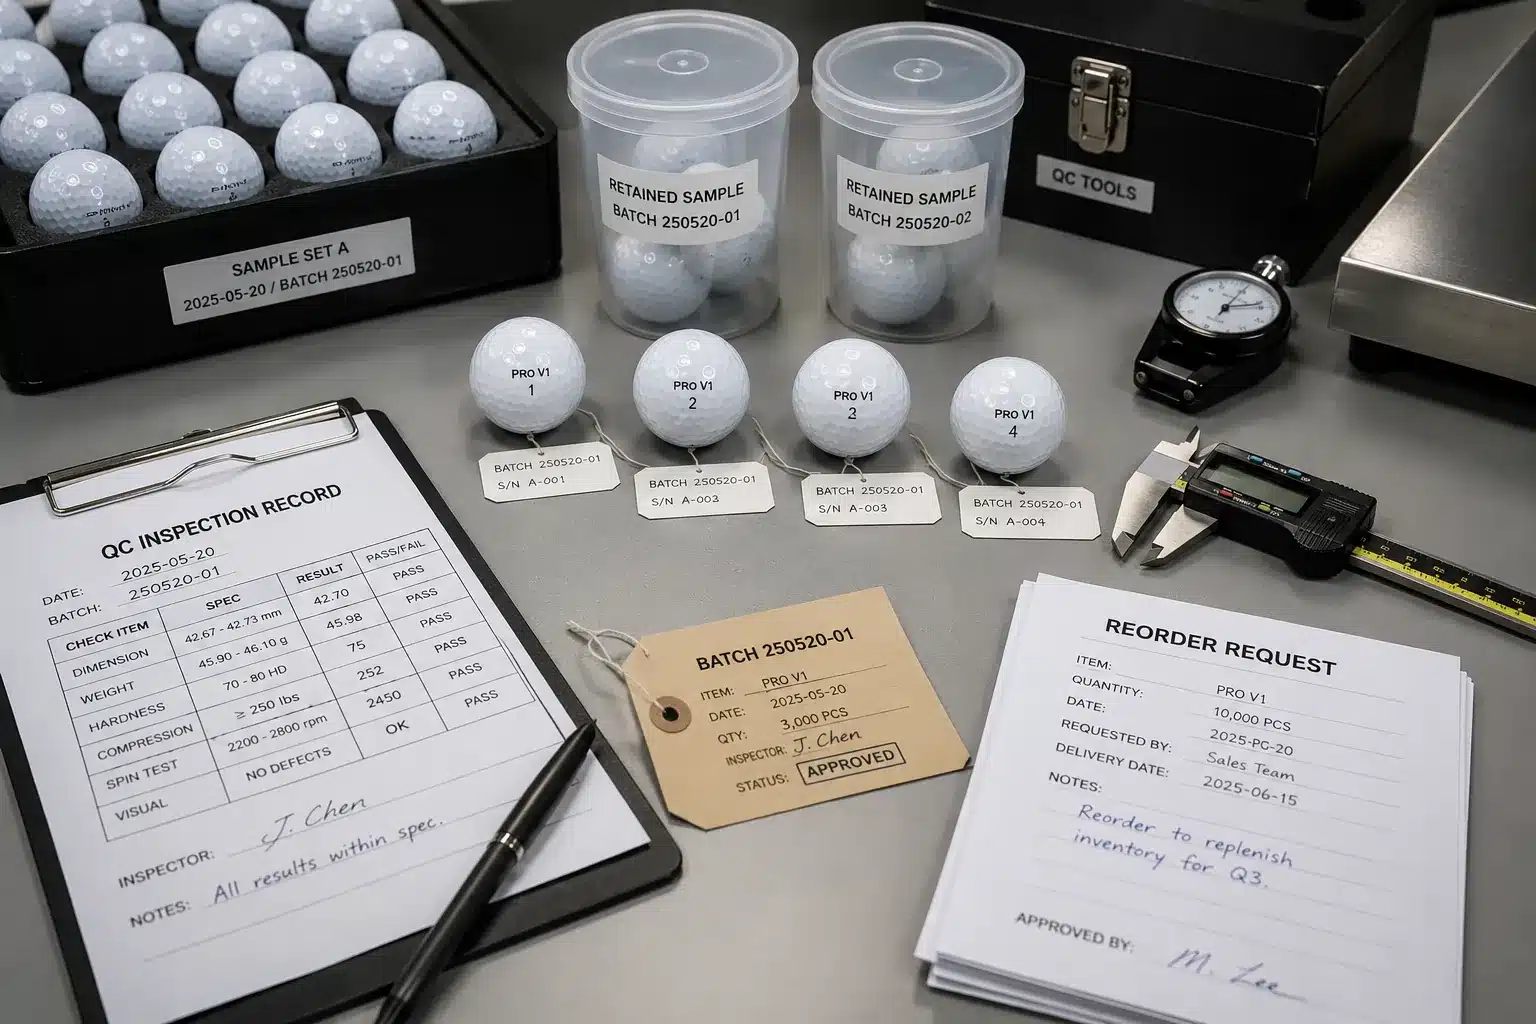
ASQ’s guidance on attribute and variable sampling provides a useful distinction for pilot QC: attribute inspection evaluates defined defect or pass/fail conditions, while variable inspection preserves numerical measurement data. Lot acceptance still answers a different question from future-lot repeatability.
Attribute evidence suits defined yes/no or defect conditions such as wrong artwork, a missing logo, visible logo bleeding, major surface defects, or packaging damage. Variable evidence suits numerical characteristics such as weight, diameter, compression, hardness, and other measured values supported by the agreed method.
| Evidence item | What it proves | Weak version | Better evidence | Buyer action |
|---|---|---|---|---|
| Approved sample | Product reference | Photo only | Sample ID + spec rev | Lock reference |
| Pilot batch | Production identity | No lot code | Batch ID | Record batch |
| Variable QC | Distribution | Average only | Raw values + spread | Keep dataset |
| Attribute QC | Visible conformity | “Looks good” | Defined checks | Define rule |
| Measurement | Comparability | Unknown tester | Method + equipment ID | Record method |
| Retained sample | Physical reference | None | Labeled sample | Preserve sample |
| Reorder | Repeatability | “Same as before” | Prior reference cited | Link next PO |
For variable measurements, preserve individual values along with the mean, range, and standard deviation where applicable. An average alone can hide a wide within-lot spread, so your reorder comparison should preserve both the center and the variation of the data.
In Golfara’s actual pilot workflow, the production batch is tied directly to the customer contract number. For example, if the contract reference is GF2026-056GFG, that same reference identifies the corresponding production batch and links it to the relevant specification and QC records.
Golfara also retains at least six balls from each production batch for a minimum of 12 months. The approved specification, batch reference, QC record, and retained balls therefore form one traceable production baseline rather than separate files with no clear relationship.
When a reorder is prepared, your team can return to that baseline instead of relying on an instruction such as “make it the same as last time.” The specification shows what was approved, the batch reference identifies what was produced, the QC record shows what was measured, and the retained balls provide a physical comparison reference.
That is what makes the first PO useful beyond the first shipment: it leaves a controlled reference that the next production batch can be compared against. If a controlled specification or production route changes, the change should be identified and approved before the previous pilot reference is reused.
Measurement comparability matters as well. NIST’s measurement-process guidance covers repeatability, reproducibility, calibration, and measurement stability. Where practical, preserve the test-method revision, equipment ID, calibration status, operator or laboratory, relevant conditioning, measurement date, and pilot lot reference.
If the sample and reorder were measured under different conditions, check the measurement change before treating a small numerical difference as proof that production changed.
A “QC Passed” statement with no batch-linked raw data, sample identity, or method reference is a failure signal.
For pilot approval, ask the supplier to identify the approved specification revision, sample reference, production route, tooling reference where applicable, batch ID format, QC evidence format, test-method reference, retained sample reference, and the changes that would require buyer reapproval before the same pilot baseline can be reused.
✔ True — A pilot can pass its lot-acceptance rule and still leave weak reorder evidence
Lot acceptance answers whether the sampled lot met the agreed rule. Repeatability requires a controlled reference that later production can actually be compared against.
✘ False — “One average value or one PASS line proves the process is stable”
An average can hide spread, and one pilot lot cannot establish long-term manufacturing stability. Preserve the evidence and build history across reorders.
When Should You Scale Beyond the Pilot?
A larger order can look attractive because the unit price drops, but a cheaper unit is not proof that your market wants the SKU or that the supplier can reproduce it.
Scale only after your pilot passes both the Market Gate and the Manufacturing Gate. Customer demand, channel feedback, and margin must support the next PO, while the supplier must also reproduce the approved product, preserve batch-linked evidence, and give the reorder a controlled reference.
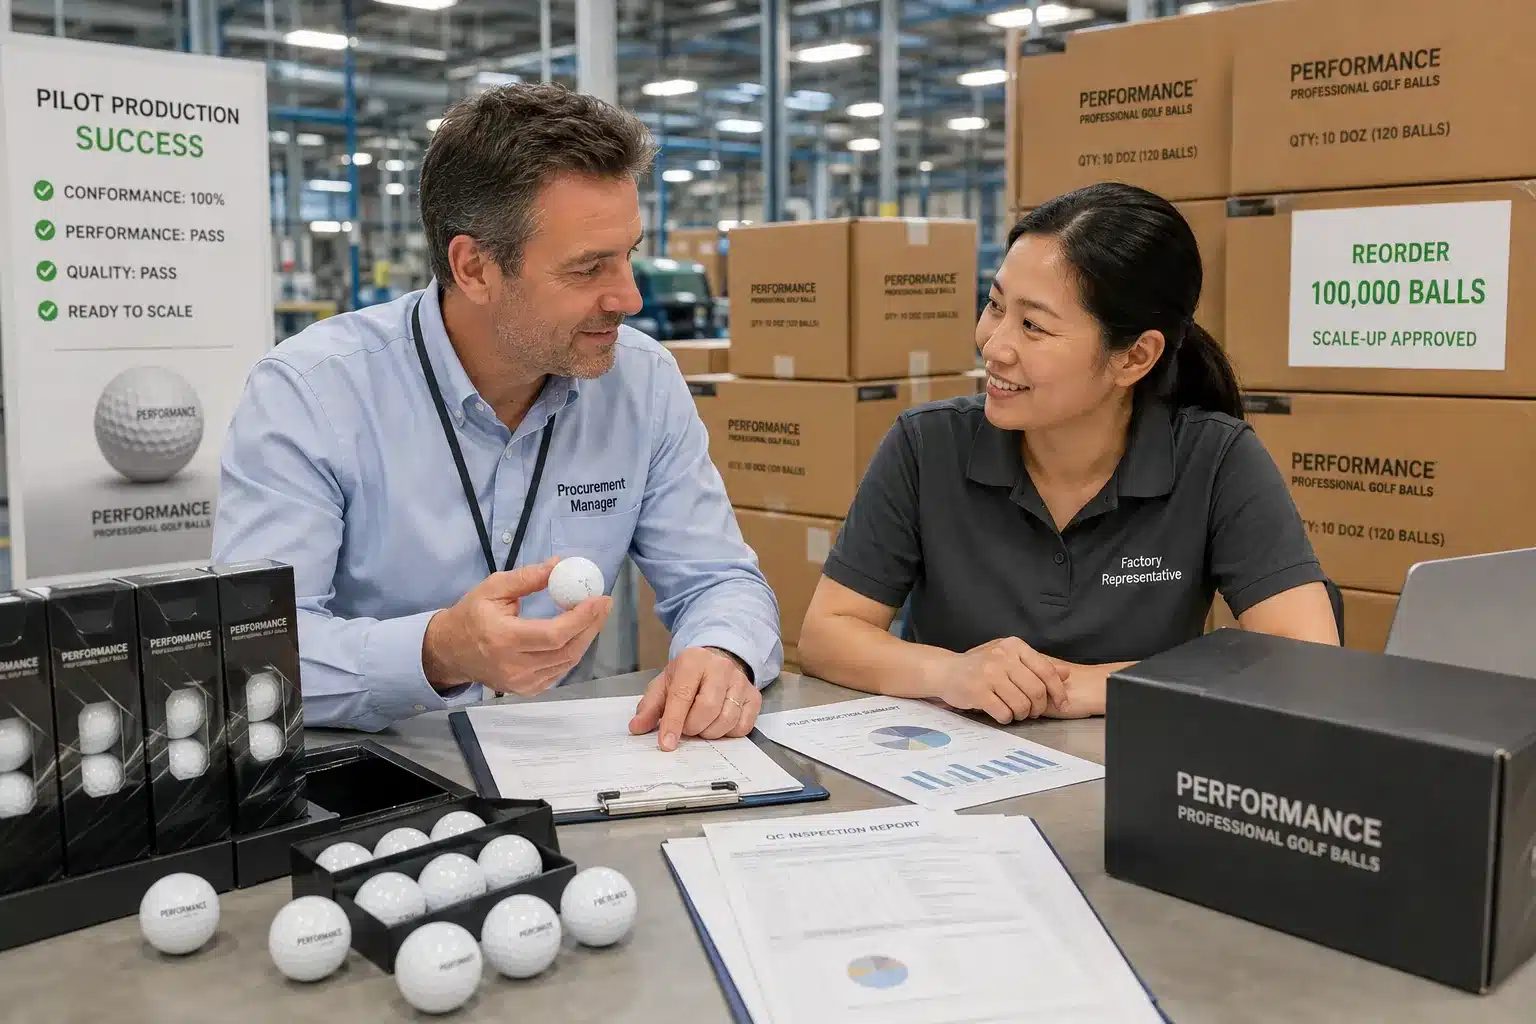
Scale because the pilot proved demand, not because the supplier offered a cheaper unit price.
For the Market Gate, review the criteria set before launch: sell-through, distributor response, channel fit, complaint records, realized margin, and genuine reorder inquiries. Do not promise 50,000 or 100,000 future pieces simply to make a 1,000-piece first order more attractive. A credible trigger is cleaner: if the pilot passes the agreed market and manufacturing gates, the program moves to the next quantity tier.
For the Manufacturing Gate, check five points: product representation, Spec Freeze, measurement validity, lot acceptance, and a usable historical reference for the reorder.
NIST’s process-monitoring guidance supports the broader principle that process behavior must be evaluated against evidence collected over time. A pilot lot can document the result of that production run, but it does not by itself establish long-term process stability.
Close the pilot with a record summarizing both gates, the retained sample, and the approved reorder reference. Your second PO then becomes the first real test of whether that controlled production reference can be reproduced.
Do not move to the next quantity tier until your pre-agreed market triggers and manufacturing evidence both support the commitment.
FAQ
Can I order 1,000 OEM golf balls?
Yes. A 1,000-piece golf ball OEM trial can be realistic when your program reuses a mature production platform, represents the SKU you intend to sell, and avoids unnecessary first-order development. Supplier acceptance still does not make 1,000 pieces a universal industry MOQ or a valid pilot by itself.
Confirm the existing construction, specification, tooling, finish, and production route before issuing the PO. Then ask whether the reorder can cite the same controlled reference.
Your first order is useful when it leaves more than inventory: approved sample, batch identity, QC evidence, retained sample, and an agreed reorder path.
Does a pilot need the same construction as my final SKU?
Your pilot should use the simplest proven construction that still represents the commercial SKU you intend to sell. A fundamentally different ball chosen only to reach a lower MOQ may test branding, price acceptance, or supplier communication while failing to validate the product promise your customers will actually buy.
Match the pilot to the intended player, channel, positioning, and core performance proposition. Not every decorative detail needs to be final, but the core product should remain representative.
If the pilot differs materially from the final SKU, document the difference and state clearly what the pilot does—and does not—validate.
Can I change the spec after approving the pilot sample?
Yes, but a material change can invalidate part of the pilot reference. Your supplier should identify whether the revision requires a new approval, updated sample, different production route, revised QC evidence, or a new development step before the changed specification becomes the new production baseline.
-
Maintain a Revision ID.
-
Record what changed and why.
-
Require buyer reapproval before production.
-
Update the sample and reorder references when the controlled baseline changes.
Without version control, your team may later blame production for a difference that actually came from an approved specification change.
What evidence should identify the pilot batch?
Your pilot file should connect the production lot to the approved product and the evidence used to accept it. A batch number provides traceability, but meaningful future comparison also needs the approved sample ID, specification revision, QC evidence, test-method reference, and retained sample ID.
-
Link the batch to the approved specification.
-
Preserve individual variable data where applicable.
-
Record the inspection or measurement method.
-
Label the retained sample to the same pilot reference.
A good file should let someone who did not manage the first order understand what was approved, produced, checked, and retained.
Can I use the pilot batch as the reference for my reorder?
Yes, if the pilot represented the intended product and production route and its evidence was preserved. The reorder should cite the pilot batch, approved specification, and retained sample, while any material change should be recorded separately rather than hidden behind vague wording such as “same as last time.”
-
Cite the previous pilot reference in the reorder PO.
-
Keep the retained sample available for comparison.
-
Reuse the same measurement basis where practical.
-
Record approved changes before interpreting batch differences.
The pilot becomes valuable when it reduces uncertainty on the second PO.
When does a pilot become new product development?
A golf ball OEM pilot begins moving into new product development when the first run requires new product architecture, formula, tooling, dimple system, cover route, or a new performance target instead of reusing a mature production platform. Quantity alone does not decide whether the project is a pilot or development.
-
Identify which elements already exist.
-
Separate new tooling or formula work.
-
Confirm whether the intended scale route is already proven.
-
Requote genuine development on its actual scope.
Do not force new development into a low-MOQ promise simply because the first order is small.
Conclusion
A 1,000–3,000-piece golf ball OEM order becomes a useful pilot when it represents the product you intend to scale, reuses a proven production platform where possible, freezes the right references, and leaves evidence your team can use for the reorder.
The quantity is only the starting point. The practical sequence is Reuse → Freeze → Prove.
If the Market Gate supports demand and the Manufacturing Gate supports repeatability, your next PO has a defensible reason to scale.
You might also like — Why Do Reordered Golf Balls Feel Different?